Bubble Sensor Factory Production Methods That Improve Sensor Reliability
2026-11-16
A bubble sensor can look flawless on a datasheet and still fail in the field because of how it was made. At Siansonic, we treat production methods as a core part of sensor reliability, not an afterthought. From controlled cleanroom assembly and precision bonding to batch-level stress screening, each step removes the hidden variability that shortens sensor life. This post walks through the factory techniques that actually move the needle on repeatability, drift, and long-term stability.
Cleanroom Airflow Patterns That Protect Bubble Sensor Membranes
Protecting a bubble sensor membrane starts with controlling how air actually moves, not just how clean the room is. A unidirectional downflow keeps particles drifting away from the sensor face, but the velocity profile matters more than the average air change rate. If the stream hits the membrane directly or creates small vortices around the mounting bracket, the thin film can flutter, stretch, or dry unevenly. Many cleanrooms run higher airflow than necessary, which sounds safer but often turns a quiet laminar field into a source of low-level turbulence right at the sensor.
Placement is the second half of the problem. Sensors tucked into an equipment exhaust wake, near a door, or just below a diffuser joint tend to see fluctuating pressure loads even when the room average looks stable. A small baffle or recessed housing can shield the membrane from direct jets, but only if it does not create a stagnant pocket where particulate or condensate collects. The goal is to let clean air wash gently past the sensor rather than pound against it.
Return air paths also shape membrane life. If the sensor sits in a dead zone near a corner or between large tools, slow-moving air can allow residue to settle and alter surface tension. A modest negative pressure gradient toward the return keeps the local environment flushed without exposing the membrane to high shear. Simple smoke tests or velocity mapping around the actual installation usually reveal problems that a room-level certificate will miss.
Inline Calibration Checks That Catch Sensitivity Drift Before Shipment
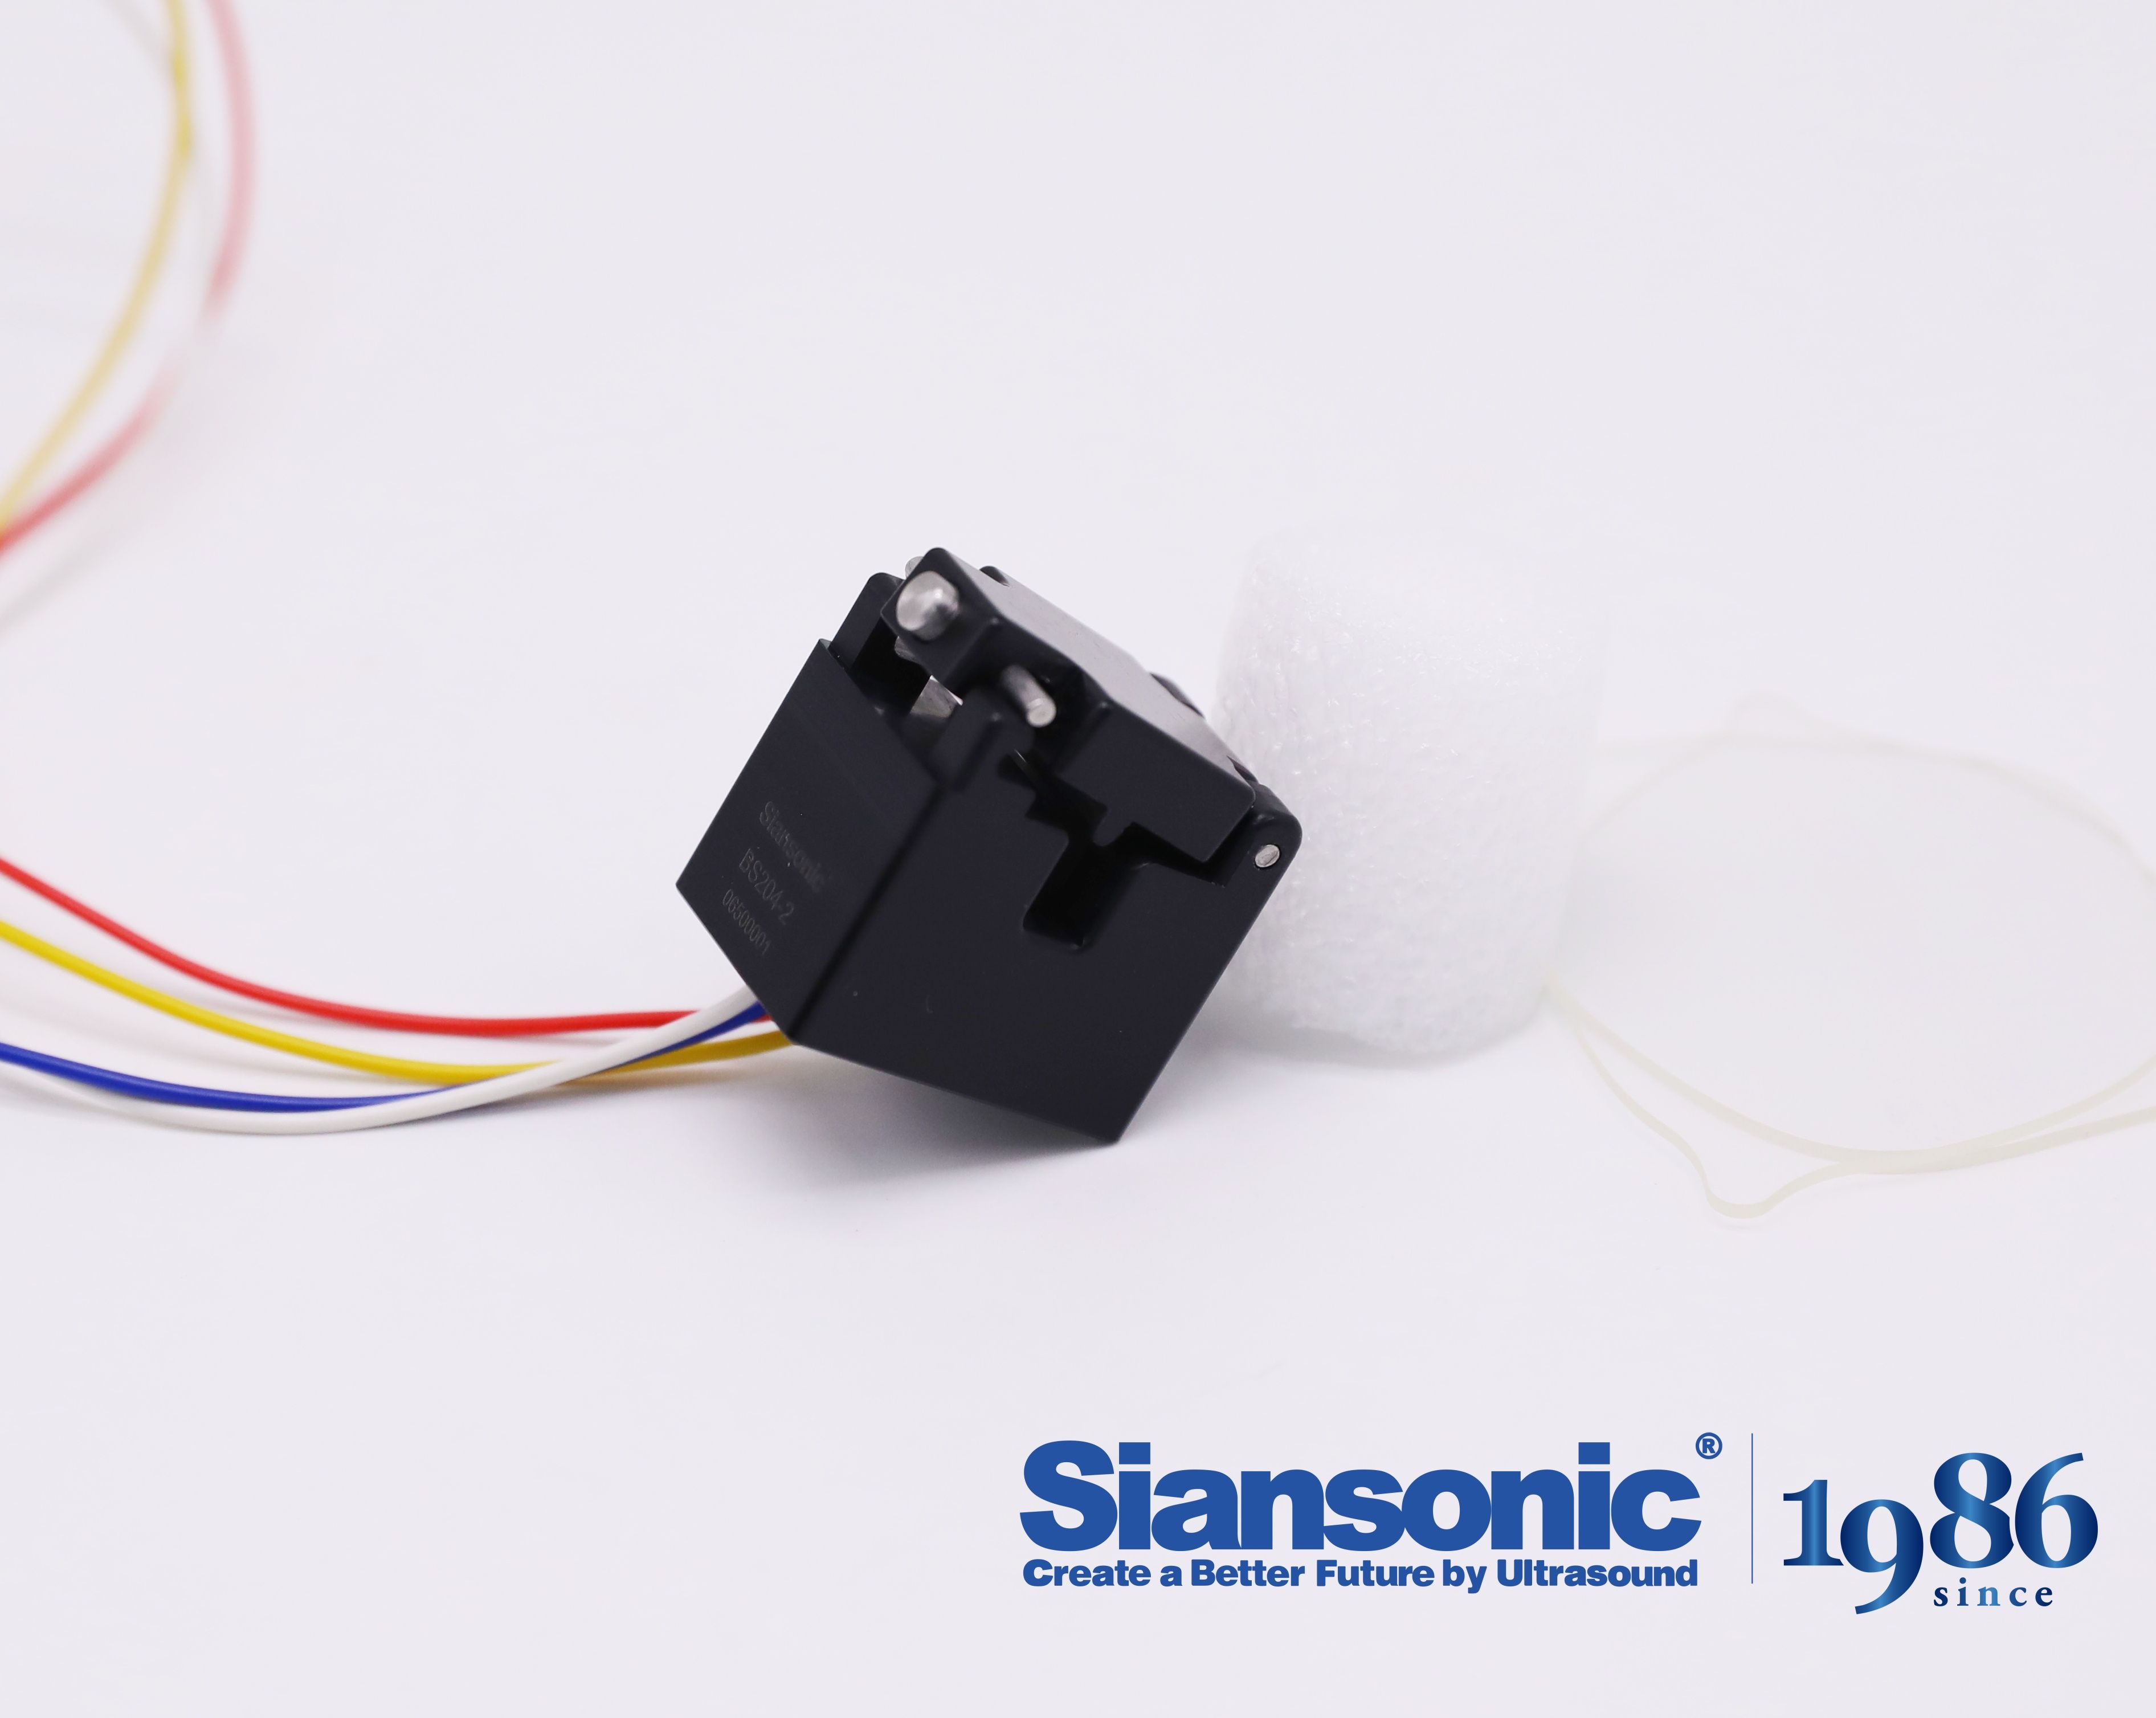
Sensitivity drift rarely announces itself. A batch of sensors can pass final bench tests while one unit sits a few millivolts outside its expected slope because the reference gas was slightly warmer than the previous run. Inline calibration checks close that gap by comparing each device against a traceable reference at multiple points along the production line, so the drift is caught while the unit is still in the test fixture, not when a customer installs it.
The checks run between coating, assembly, and final packaging rather than as a single gate at the end. When a unit starts trending toward the edge of its allowed span, the line stops it for a quick re-zero and span adjustment. That matters most for low-ppm electrochemical cells and optical sensors, where a small baseline movement can turn into a false alarm or a missed exposure in the field.
Every check writes pre/post values to the unit's serial record, which gives manufacturing a clear view of which stations introduce the most variation. It also means the customer receives a unit that has already demonstrated stable response before it leaves the dock.
Material Pairing Decisions That Reduce Fluid Contamination Risks
Contamination in a fluid system is rarely just an ingression problem. A large share of downstream failures starts with the materials themselves: a zinc-plated fitting in contact with a phosphate ester, a polyurethane seal in a high-acid bio-oil, or a copper alloy exposed to sulfur-bearing gear oil. These pairings can generate metal soaps, hydrolysis fragments, or corrosion debris that are far harder to remove than ordinary dirt. Replacing the zinc plating with electroless nickel and switching the seal to a fluorocarbon often reduces particle counts more effectively than adding another filter stage.
Seals and hoses deserve closer scrutiny than their temperature ratings suggest. Many elastomers slowly release plasticizers or low-molecular-weight fractions when they sit in aggressive additives, and those extracts can settle in tiny orifices or contaminate precision surfaces. In some cases, the safer choice is not the highest-performance polymer but the one with the lowest extractable content under your specific fluid chemistry. Metal pairs matter too: coupling stainless steel with bare aluminum in a wet environment can drive galvanic corrosion that feeds soluble ions back into the stream, changing conductivity and accelerating oil breakdown.
A short immersion test usually reveals more than a stack of datasheets. Place candidate seals, fittings, and hoses in the actual working fluid at peak operating temperature for several weeks, then check hardness, mass change, color shift, and filter residue. If two individually acceptable materials create deposits only when used together, changing one side of the pair is almost always a better fix than compensating with finer filtration.
Low-Stress Assembly Methods That Preserve Thin-Film Sensing Layers
Thin-film sensing layers rarely fail during operation; it is usually assembly that does the damage. Even small mismatches in pressure, temperature, or flatness can crack a sensor or shift its baseline once the device is bonded to a substrate. Low-stress methods keep the film away from direct clamping force and use adhesives that cure close to room temperature, so the layer never sees the thermal swings that cause delamination.
One approach is to place the sensor near the neutral bending plane of the stack, or to use a thin elastomeric interlayer that absorbs localized pressure before it reaches the sensing film. Anisotropic conductive film can work well when the bonding profile is tuned to stay below the film's degradation threshold. For particularly fragile coatings, transfer printing with a soft stamp avoids pressing rigid tooling against the active area altogether.
The real test is whether the sensor still drifts, cracks, or peels after thermal cycling and flexure. Checking resistance stability, adhesion at the edges, and surface morphology under a microscope often catches problems that electrical tests miss. In practice, combining low-cure adhesives, compliant underfills, and matched expansion coefficients gives the sensor a better chance of surviving both assembly and the lifetime that follows.
End-of-Line Testing With Real Fluids, Not Just Air
Air-based checks at the end of a production line can tell you whether a passage is blocked or grossly leaking, but they stop well short of how a component actually behaves under service conditions. Viscosity, surface tension, and even the way a liquid foams or clings to internal walls change the pressure signature in ways dry gas cannot replicate. Swapping to real fluids — the actual coolant, brake fluid, fuel, or oil the part will carry — turns a basic pass/fail check into a meaningful functional test.
The differences show up most clearly around small orifices and tight clearances. A part that holds 50 psi of air without any audible hiss may still seep fluid at 2 psi because the liquid wets the seal interface and follows microscopic leak paths. Running production samples with the intended fluid also catches issues like seal swell, elastomer compatibility, and trapped air pockets that only appear after the first wetting cycle.
Practically, this means the test bench needs a different layout: fluid reservoirs, filtration, temperature control, and a recovery system to keep costs and mess under control. It is slower than an air test and demands stricter cleanup between cycles, but the payoff is a much lower chance of shipping a part that passes on the bench and fails in the vehicle or machine a week later.
Lot-Level Traceability That Pinpoints Production Variability Fast
When a batch drifts out of spec at 2 a.m., the difference between a ten-minute fix and a two-day investigation often comes down to how cleanly lot data is linked to process readings. Lot-level traceability lets teams follow the exact raw material lots, machine settings, and operator adjustments tied to a specific run, so a viscosity shift or a slight seal-pressure change shows up next to the batch number instead of being buried in a shift log.
On a filling line, that means a quality engineer can pull up one lot and see that the filler nozzle was recalibrated mid-run, or that two pallets of resin from a secondary supplier entered just before rejects climbed. Because comparisons happen lot by lot instead of in aggregate, the conversation shifts from a vague sense that something changed recently to a checkable pattern across three specific lots. That speed matters most when downstream customers are waiting, or when the same variability risk may still be sitting in other batches in inventory.
FAQ
The removal of trapped air from the sensing gel or adhesive layer. Even sub-microliter voids create nucleation sites that expand with temperature swings. We switched to a two-stage vacuum degassing process and cut field failures by roughly a third.
Replacing standard silicone potting with a low-outgassing fluorosilicone has made the biggest difference. It keeps the optical path clear, reduces drift, and survives humidity cycling far better than the cheaper compounds.
We moved sputtering to a heated substrate stage and added a slow post-deposition anneal. The thermal mismatch between the film and the polymer substrate is the main culprit; letting the film relax before exposure to room air prevents most hairline fractures.
Sensor response shifts during the first few hours as adhesives cure and residual stress settles. If you calibrate immediately, the baseline moves later and the sensor drifts out of spec. Waiting 24 to 48 hours at operating temperature gives a much more stable reference.
We use a low-frequency impedance sweep while the sensor is submerged. A healthy sensor shows a smooth, repeatable phase curve. Small delaminations or pinholes show up as irregular jumps before the sensor ever fails a standard bubble test.
Tight control of the coating thickness near the electrode edge has the biggest impact. We use a narrow-band optical reflectometer on every wafer and reject anything outside a 2 micron window. That single change dropped batch-to-batch variability more than any other process adjustment.
For exposed sensing surfaces, yes. Particles embed in the membrane and create weak points where microbubbles collect. We run the final assembly in an ISO 6 area and use ionized air to reduce static attraction; contamination-related rejects fell sharply after the upgrade.
Hard epoxy at the cable entry. Any cable movement transfers stress directly to the solder joints or the sensor substrate. A softer strain-relief compound and a reinforced boot solve most of those failures without touching the sensing design.
Conclusion
At the production floor, reliability starts long before a bubble sensor is sealed into its housing. Cleanroom airflow is arranged so that filtered air sweeps across open membrane areas rather than pushing particulates into them; even small shifts in velocity or return-air placement get flagged because they show up as membrane defects. Material choices are handled as a compatibility question, not a simple cost trade-off. Adhesives, gaskets, and carrier films are screened for extractables and leachables against the fluids that the sensor will contact, which prevents slow chemical attack or residue buildup from reaching the thin-film layer. Assembly fixtures use controlled force and thermal profiles, so the sensing films are never stretched, crimped, or heated past the point where their output begins to drift.
Before shipment, each lot moves through inline calibration checks that compare response against reference solutions at multiple set points; if sensitivity starts to move, the lot is stopped before it reaches packaging. End-of-line testing uses the actual fluids the customer will monitor, which catches bubbles, wetting differences, and surface effects that air-only tests miss. Lot-level traceability ties each sensor to raw material batches, fixture settings, operator shifts, and test records, so when variation appears, it can be traced to a specific workstation or supplier lot instead of becoming a recurring field problem.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/