China Resin 3D Printer Company Drives Next-Gen Additive Manufacturing with High-Precision Solutions
2026-09-28
In the fast-evolving landscape of additive manufacturing, few players are pushing the boundaries quite like ProtoMat. As a China-based resin 3D printer specialist, ProtoMat is rewriting the rules of precision—turning next-gen ideas into tangible, high-resolution reality. This post dives into how their latest high-precision solutions are not just keeping pace with industry demands, but setting a new bar for what resin-based printing can achieve.
Where Micron-Level Accuracy Meets Production Tempo
Manufacturing has long forced a frustrating trade-off: chasing micron-level precision usually means slowing down, while cranking up speed invites cumulative drift. That line is being redrawn.
By integrating high-resolution feedback loops with adaptive compensation algorithms, the system self-corrects multiple times per second without human intervention. The motion-control architecture has been rebuilt to eliminate lag from thermal drift and vibration, making each move both decisive and exact.
The result is a line that no longer has to choose between doing it right and doing it fast. Cycle times drop while yield climbs, and changeovers no longer trigger lengthy recalibration. Microns stop being a lab luxury and become a floor-level constant.
Resin Chemistry Choices That Shape Final Part Performance
The backbone of any high-performance resin lies in its polymerization pathway—whether it's a step-growth epoxy, a condensation-cured phenolic, or a free-radical vinyl ester. Each route imposes a distinct network architecture: epoxy's oxirane rings open into tight, cross-linked lattices that resist creep under load, while unsaturated polyesters lean on styrene bridges that trade some thermal stability for easier processing. What often gets overlooked is how the choice of catalyst or initiator tunes the final morphology. A slow amine cure might yield larger, more ordered domains that improve fracture toughness, whereas a rapid peroxide kick-off can trap internal stresses that later manifest as micro-cracking. These subtle shifts in reaction kinetics are what separate a part that survives thousands of thermal cycles from one that embrittles after a single season outdoors.
Beyond the base chemistry, the pendant groups and backbone flexibility dictate how a finished part behaves when the environment turns hostile. Aromatic rings in bisphenol-A epoxies provide rigidity and high glass transition temperatures, making them ideal for under-hood automotive brackets, but the same structure can become brittle at sub-zero temperatures unless toughened with carboxyl-terminated butadiene or core-shell rubbers. On the other end, cycloaliphatic resins offer superior UV resistance and low viscosity for potting electronics, yet they demand careful stoichiometry to avoid unreacted monomers that leach out over time. The art is in matching the resin's molecular personality to the part's real-world duty cycle—not just chasing datasheet numbers like tensile modulus or heat deflection temperature, but asking how the chemistry will age under moisture, chemical exposure, and repeated stress reversals.
Finally, the interface between resin and reinforcement or filler is where many performance promises quietly fail. A resin with excellent bulk properties can still delaminate from glass fibers if the silane coupling agent doesn't bridge the organic-inorganic gap, or if the resin's shrinkage during cure pulls the matrix away from the fiber surface. Toughened systems often sacrifice a bit of stiffness to gain adhesion through polar functional groups that hydrogen-bond with oxidized metal or treated carbon. Additives like wetting agents, defoamers, and even trace amounts of water scavengers further sculpt the final part's surface energy, void content, and long-term durability. In practice, the winning formulation rarely hinges on a single exotic monomer—it's the cumulative effect of dozens of small chemistry decisions, each nudging the part toward either silent failure or years of reliable service.
Inside the Build Chamber: Managing Light, Heat, and Repeatability
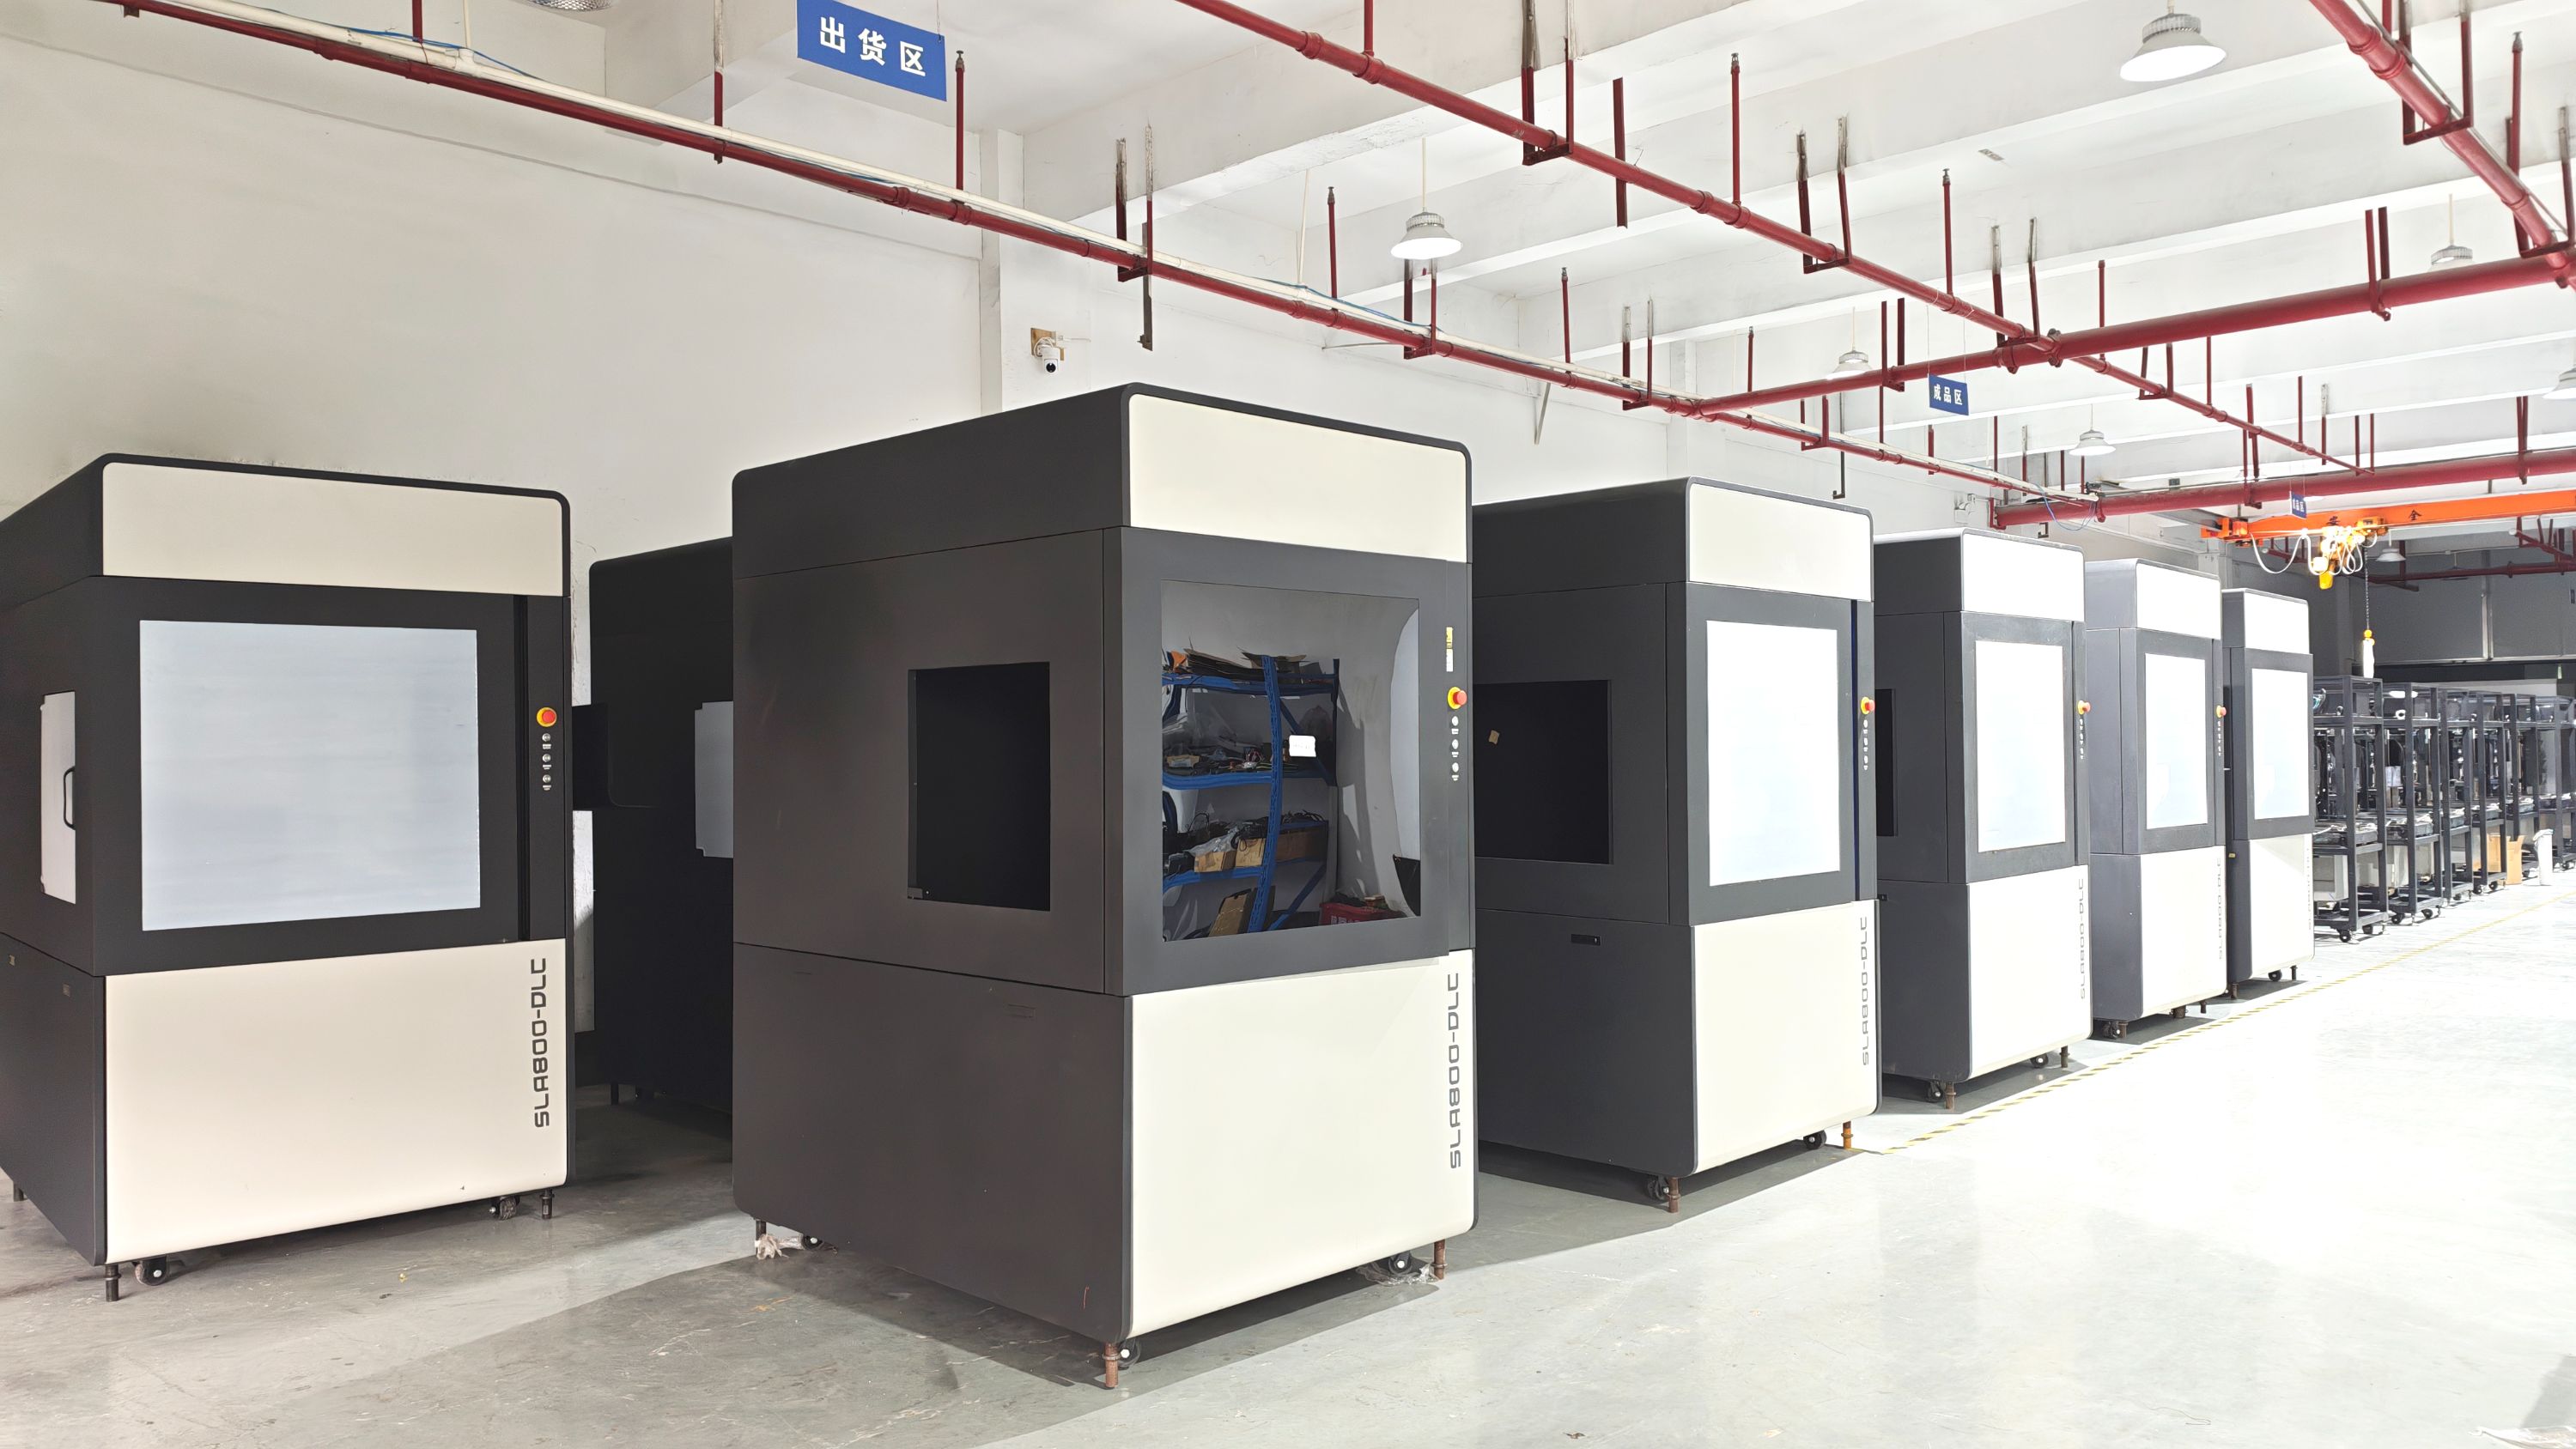
Most people assume the projector is the only light source that matters, but inside a resin printer’s build chamber, stray UV from the curing lamp or even sunlight through a window can ruin a print before it starts. The enclosure isn’t just a dust cover—it’s a controlled environment. We kept the interior matte black to absorb incidental reflections and added a sealed lid that blocks ambient UV without trapping so much heat that the resin thins out mid-print.
Heat management is the part nobody talks about until a tall print fails at hour six. As the light engine runs, the chamber temperature creeps up, and that can change how each layer cures. We mounted a small thermistor near the build plate and tuned the cooling vents to keep the temperature swing under two degrees Celsius across a full build. The result is repeatability that shows up in the last layer exactly like the first.
From Dental Models to Jigs: Real Workflows, Not Just Demo Prints
Printing a dental model is often treated as the finish line, but in a working lab or clinic it’s only the starting point. The real job begins when that model becomes a seating jig for implant planning, a drill guide for guided surgery, or a try-in for a temporary restoration. If the printed arch doesn’t capture the gingival contours, adjacent tooth contacts, and prepared margins accurately, every downstream step inherits that error. So the workflow has to be built around measuring fit at the model stage, not just eyeballing a shiny print.
The gap between a clean demo print and a production-ready jig shows up quickly once you start checking things like intaglio surface adaptation, sleeve alignment in surgical guides, and how the resin behaves after repeated autoclave cycles. Many shops waste days tuning support structures or reprinting because they didn’t decide on print orientation and drain holes before hitting slice. A better approach is to maintain a small library of validated settings for each resin and jig type, then run a fit test on a known master model before committing to patient-specific work.
Real workflows also mean accepting that cleaning and post-curing are not afterthoughts. A guide that looks perfect off the build plate can warp during drying if you rush the IPA bath, or become brittle if the curing time is guessed. The teams that get consistent results treat printing as a production system: they document orientation, support density, wash time, cure temperature, and verify each batch against a go/no-go gauge. That shift from demo prints to repeatable jigs is what actually keeps chairs on schedule.
Why Calibration Routines Matter More Than Resolution Specs
The spec sheet loves to shout about pixels—4K, 5K, 8K—but those numbers mean little if the panel can't show a neutral gray at 50% brightness. Calibration routines fix the stuff resolution can't touch: color temperature, gamma response, and channel balance. A monitor with a lower native resolution but a consistent calibration process will render skin tones and shadows more truthfully than a high-res panel left at factory defaults.
Resolution is a fixed attribute. You buy it once, and it never changes. Calibration, on the other hand, is not a one-and-done task. Backlights age, color filters shift, and even room lighting drifts with the seasons. Without a routine—weekly for critical work, monthly for casual use—your display slowly falls out of spec. That's why a repeatable calibration habit ends up mattering more than the pixel count printed on the box.
I've seen photographers edit on a 4K screen that hadn't been calibrated in a year. The prints came back magenta-skinned. Meanwhile, a properly calibrated 1080p display produced accurate, predictable results. It's not that resolution is worthless; it's that calibration is the layer that keeps every one of those pixels honest. If you have to choose between the two, the calibration routine wins almost every time.
Scaling a Printer Line Without Diluting Quality
Growth usually tempts you to speed up every stage, but that's exactly where print defects start. Instead of rushing setup times or pushing higher throughput on existing machines, we found it better to scale by duplicating proven stations rather than stretching them. Keep the same hardware, same maintenance cadence, same calibration steps—just add another line once the first one hits a stable quality baseline. That way, quality is replicated instead of renegotiated.
Material consistency gets harder as volume climbs. A supplier that was fine for small batches may struggle to keep lot-to-lot viscosity or particle size within tight limits when orders triple. We hold weekly incoming checks on a few critical properties and reject any batch that falls outside the band, even if production is waiting. That discipline feels expensive for an hour, but it prevents weeks of troubleshooting invisible print defects later.
New operators pose the biggest dilution risk during scale-up. Instead of relying on a few senior technicians to catch problems, we embed quality checks directly into the line: inline cameras, automated viscosity logs, and pass/fail test strips at each shift. This doesn't replace skilled judgment, but it gives new hires a safety net while they build enough experience to notice subtle drift.
FAQ
They combine advanced optical systems with tightly controlled resin formulations, achieving layer resolutions down to 25 microns while maintaining dimensional accuracy across large build volumes.
By using a proprietary light engine that cures entire layers uniformly, the printers deliver smooth surfaces and fine details without slowing down production cycles.
Dental labs, jewelry makers, and microfluidic device manufacturers gain the most, as they need intricate geometries and repeatable tolerances that conventional resin printers struggle to produce.
They are built for both. Automated resin handling, long-life consumables, and stable calibration allow continuous operation for small-batch production, not just one-off prototypes.
The company offers bio-based resins and a closed-loop filtration system that reduces waste by reusing uncured material, cutting both environmental impact and operational costs.
It provides on-demand calibration profiles, a curated resin library, and direct engineering support, so teams can transition from design to reliable prints without a steep learning curve.
Custom slicing algorithms automatically compensate for light scattering and shrinkage, and adaptive support generation minimizes post-processing damage on delicate features.
The region benefits from dense supply chains for optics and photopolymers, plus rapid iteration cycles, allowing companies like this one to push resolution and reliability faster than many overseas peers.
Conclusion
Across its latest resin printer lineup, the company pairs sub-25-µm feature resolution with throughput figures usually reserved for far less precise machines. This is not a spec-sheet contest, though. The real differentiation comes from how different acrylate and epoxy blends are matched to end-use demands—high fracture toughness for snap-fit jigs, low ash content for burnout dental models, rigid clarity for fluidic manifolds—rather than forcing a single universal resin on every application. Inside the build chamber, the engineering is deliberately unglamorous but decisive. Uniform light intensity across the entire vat, active thermal stabilization of the resin tray, and closed-loop feedback on peel forces keep layer-to-layer variation below what most datasheets even disclose. That consistency is what lets a dental lab run overnight queues of surgical guides without an operator hovering nearby, and lets an electronics manufacturer trust that the 200th connector housing will seat as cleanly as the first.
What separates this approach from demo-led marketing is the focus on dirty, real-world workflows. The same machine that holds a 50-micron margin line on a crown also cranks out assembly jigs for an automotive tier-one supplier, with changeover measured in minutes, not shifts. The company's field engineers spend more time on calibration routines—mapping resin shrinkage per batch, verifying z-axis orthogonality under thermal load, logging LED output drift over hundreds of hours—than on quoting raw pixel counts. That discipline carries through to manufacturing scale. New production lines for the printers themselves mirror the repeatability of the machines: incoming optics are batch-tested against a golden reference, gantry assemblies are laser-aligned before leaving the floor, and software builds are frozen unless a stress test shows zero regression. The result is a printer family that does not ask users to choose between precision now and reliability next year, and that quietly raises the bar for what resin additive manufacturing can promise outside a trade-show booth.
Contact Us
Contact Person: Joe
Email: [email protected]
Tel/WhatsApp: +8613799507208
Website: https://www.3dprotomat.com/