China Thread Button Bit Factory Delivers Premium Rock Drilling Tools Worldwide
2026-09-26
Rock drilling rarely forgives shortcuts. The thread button bits spinning at the end of a drifter either hold their edge under brutal torque and percussion, or they send the whole crew back to the tool trailer. PULANKA understands that pressure because it builds its bits in one of China’s most demanding manufacturing environments — then ships them to drilling teams in over 40 countries. The result is a quieter, more predictable supply chain for contractors who can't afford downtime. Here's what makes that factory-to-field pipeline different.
Rock Hard? These Thread Button Bits Chew Through It
When most bits bounce off unforgiving formations, these thread button bits dig in and refuse to let go. The carbide buttons are arranged to concentrate impact exactly where it counts, so even granite, quartzite, or heavily fractured basalt gets pulverized instead of just scratched. You'll notice the difference on the first hole—less skidding, faster penetration, and a bottom-hole pattern that looks clean rather than chewed up.
What really sets them apart is how the thread design handles the punishment. Instead of loosening under constant percussion, the connection stays tight, transferring energy straight into the rock. That means fewer pull-outs mid-hole, fewer stripped threads, and a bit that keeps its edge long after conventional designs have gone dull. Crews often report finishing jobs with the same bit they started with, even in abrasive ground.
Don't let the compact size fool you. These bits are built for the kind of rock that eats lesser tooling for breakfast. Whether you're chasing water wells, blasting holes, or anchoring into hard strata, you get steady, predictable wear that lets you plan your footage instead of guessing when the next failure will hit. When the ground fights back, this is the bit that chews through it.
From Forge to Site: The Journey of a Single Button Bit
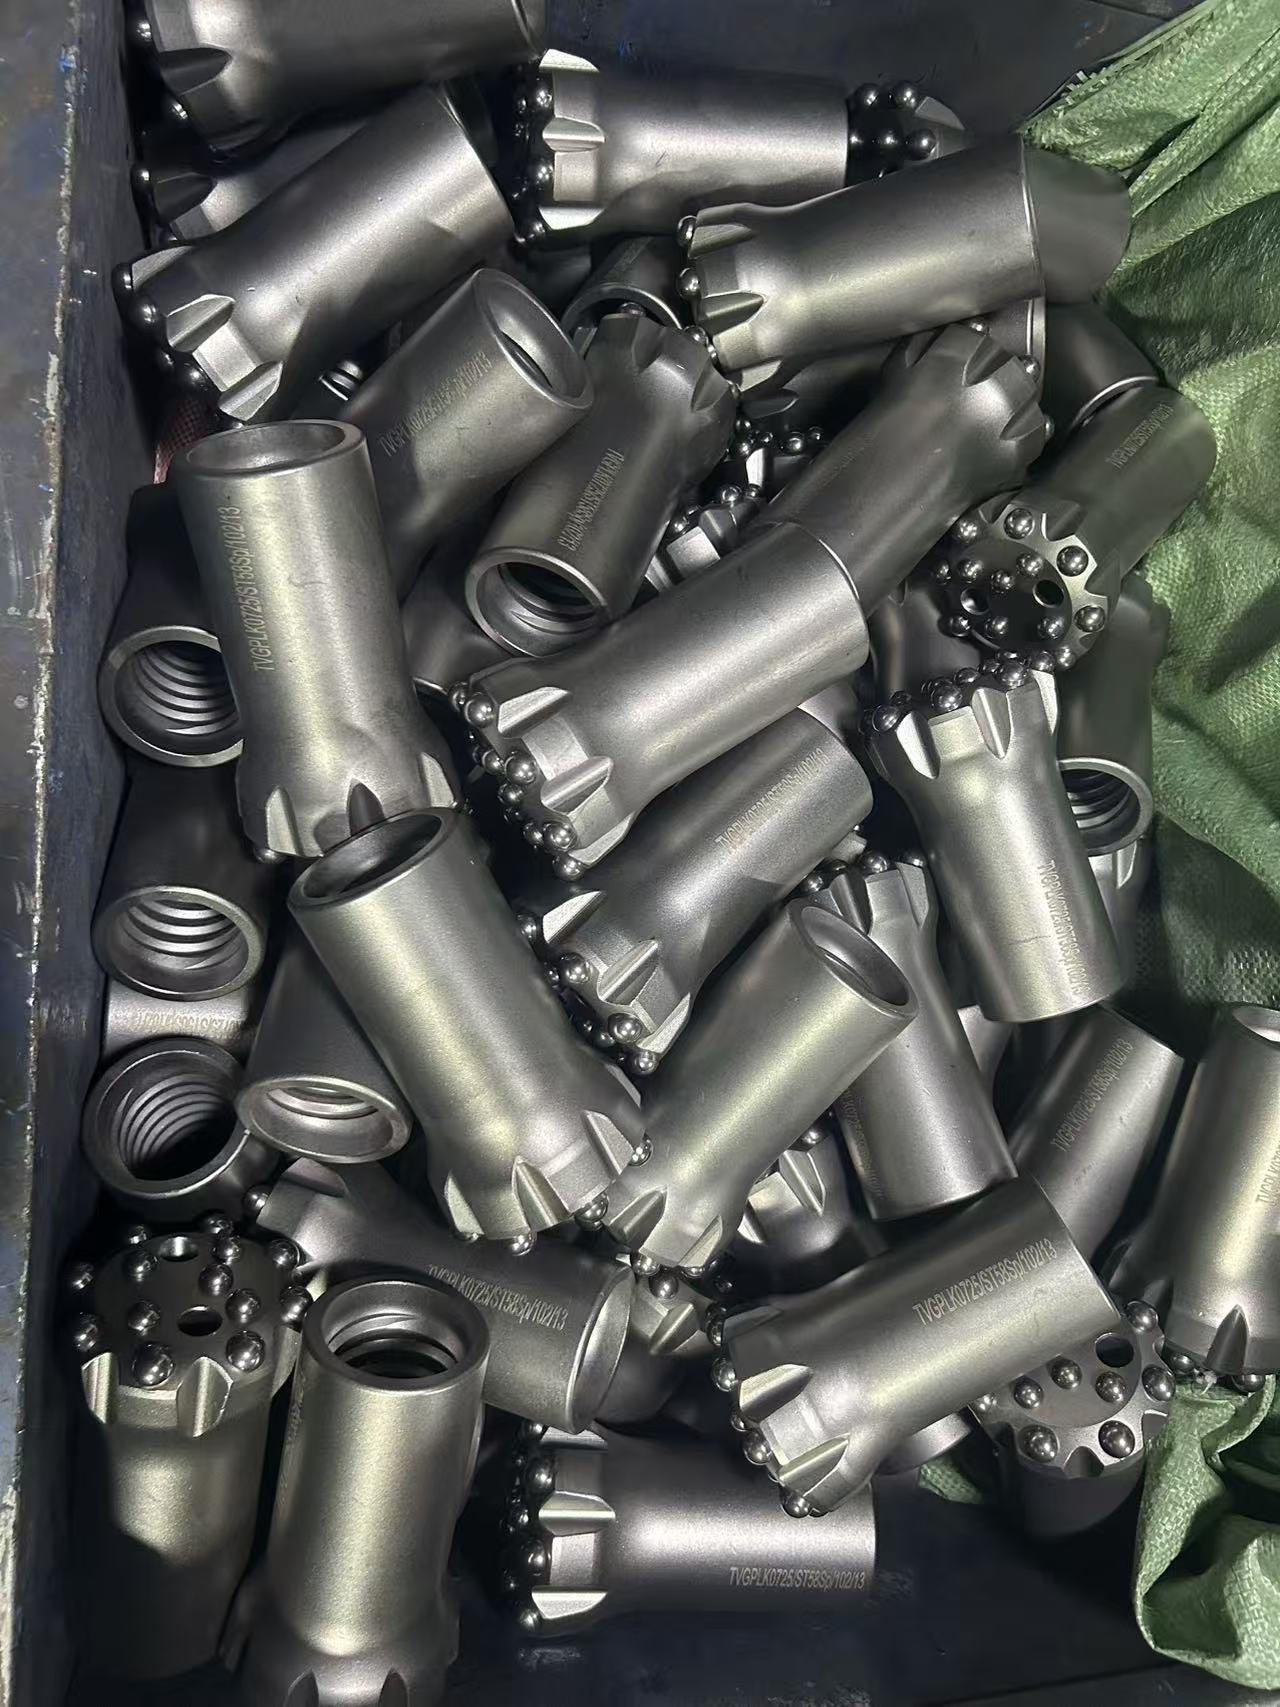
The button bit does not leave the forge as a finished tool. It starts as a blank of carefully selected steel, heated until it glows and then pressed into a rough crown shape. On the shop floor, the tungsten carbide buttons are seated into pre-drilled holes with a hydraulic press—too little force and they will shimmy loose, too much and the steel around them cracks. Once the body takes shape, the threads are cut at the base, and the bit is sent through a slow, controlled cooling. Each step leaves marks that later tell a story on site.
After grinding and inspection, the bit gets wrapped in rust-resistant paper and packed into a wooden crate with a dozen others. It might spend weeks bouncing across a supply route or waiting in a site container before a driller finally threads it onto a hammer. The first few meters underground are always a test: how well the face flushes cuttings, whether the gauge holds, if the buttons stay put. From forge to site, the bit carries the decisions made days earlier in the factory.
Custom Profiles for Quarry, Mining, and Tunneling Jobs
Every quarry face, underground drift, and tunnel heading presents its own set of ground conditions, production targets, and access constraints. That's why we don't believe in forcing a standard bucket or blade profile onto a job that demands something more specific. Instead, we work from your site surveys, blast patterns, and material flow data to develop custom profiles that match the actual wear patterns and loading geometry you deal with day after day.
From extra-deep lip shrouds for abrasive granite to reinforced heel sections for tight corner loading in narrow veins, the adjustment isn't cosmetic—it changes how the machine balances, how material rolls in the bucket, and how quickly you can cycle. We've built profiles for everything from high-volume copper pits to small-diameter sewer tunnels, and each one starts with a conversation about what's slowing you down or wearing out too fast.
The result is a ground-engaging tool that doesn't just survive the job, but actually fits the way your operators work. You get better fill factors, less spillage, fewer change-outs, and a wear package that makes sense for your specific rock type and blast size. No generic catalog numbers—just a profile that was drawn around your operation.
The Inspection Gauntlet Every Bit Must Survive
A bit rolling off the line doesn't get a free pass. It enters a corridor of lasers, load cells, and vision systems that measure edge geometry down to a few microns. Any chip, any uneven wear, any microscopic fissure and the whole piece gets pulled before it ever touches a chuck.
The gauntlet isn't just about catching defects. It's about proving the bit can handle torque spikes and thermal shock without losing its cutting edge. Testing jigs slam the bit into hardened steel again and again, while sensors track deflection and heat buildup. If a single flute fails to clear chips, the run stops.
Most bits don't make it through unchanged. That's the point. Only the ones that survive with geometry intact and coating unbroken earn a spot in the box.
Packaged for Ports, Shipped to Six Continents
Every crate that leaves our facility is built for the rough realities of dockwork, not just warehouse shelves. We size timber frames to match the exact dimensions of the machinery, add reinforced corner blocks and steel strapping where stress concentrates, and line the interior with VCI film or desiccant packs when the destination climate demands it. That way a pump headed to Rotterdam or a gearbox bound for Singapore arrives without corrosion streaks, crushed edges, or customs delays caused by non-compliant wood packaging.
The paperwork moves as carefully as the cargo. Our team preps commercial invoices, packing lists, certificates of origin, and ISPM 15 heat-treatment stamps before the truck ever backs into the loading bay. Because we label every face with handling marks, net and gross weights, and port of discharge in large stencil lettering, forklift operators and freight forwarders can route each box correctly without guesswork — whether it is transshipping through Busan or clearing in Santos.
Six continents means more than a wider map on the wall. It means we have learned which carrier accepts a 4.2-meter overheight crate without surcharge, when to switch from ocean to air freight for urgent spare parts, and how to brace internal components so they survive a week on rough roads before reaching the final plant gate. The result is the same packaging philosophy applied from the first nail to the final seal: make it strong, make it legible, make it easy to handle anywhere.
Field Reports: Why Crews Are Quietly Upgrading Their Bits
A growing stack of field notes points to the same pattern: crews aren’t waiting for the next big equipment purchase to fix slow drilling. Instead, they’re swapping in redesigned bits that hold an edge longer in mixed ground. On one road project, a foreman logged a 30 percent drop in bit changes after moving to a new carbide grade—no fanfare, just fewer stops to re-tool.
Part of the shift is driven by material advances that never made the front page. Polycrystalline diamond compact cutters and tougher binding alloys are showing up in standard sizes, letting smaller contractors get the same wear resistance that used to be reserved for high-end jobs. The upfront cost stings a bit, but the math works once you track downtime and labor per hole.
There’s also a quiet practicality at play. Many crews are testing small batches or resharpened profiles before committing, so they don’t advertise the change until the results are repeatable. In the meantime, operators report smoother feed rates and less chatter in reinforced concrete, which keeps the whole rig from taking a beating.
FAQ
They handle a wide range, from soft limestone to hard granite and abrasive sandstone. The carbide buttons and face design can be adjusted to match the ground, so you are not forcing one bit to do every job.
Yes, custom thread profiles and shank lengths are available. Send over your rig specs and drilling parameters, and the engineering team will match the connection to your hammer or drifter.
Each batch goes through hardness testing, dimensional checks, and brazing inspection. The factory keeps records for every heat of steel and carbide grade, so repeat orders perform just like the first.
Absolutely. They make retrac and button styles that reduce jamming in narrow holes. The bit body is designed to clear cuttings quickly, which helps when ventilation and maneuverability are tight.
For standard models, they keep a ready stock and can ship within a couple of weeks. For custom bits, air freight can cut transit time significantly if the project timeline is tight.
They provide usage guides, recommended rotation and feed pressure settings, and troubleshooting help over email or video call. If a bit underperforms due to a manufacturing defect, they will replace it under warranty.
It often comes down to the balance of cost and durability. The factory uses high-grade carbide and precision machining, but the production scale keeps pricing lower than many Western suppliers without sacrificing performance.
Yes, many customers regrind the buttons several times before replacing the bit. The factory can provide regrinding specifications and, in some regions, recommend local service partners.
Conclusion
Down in the borehole, where granite doesn't yield and limestone fights every rotation, these thread button bits from China's factory floor earn their keep. They're forged from high-grade alloy, then shaped to match the exact rock profile of a quarry bench, a mine face, or a tunnel heading. Each blank passes through a gauntlet of ultrasonic scans and hardness tests before it ever sees a drill rig. That's why operators who've been chewing through stone for decades notice the difference: less vibration, cleaner holes, and fewer bit changes per shift.
Once a bit survives inspection, it's packed in rust-resistant crates and shipped from coastal ports to job sites on six continents. Field reports trickle back from crews in the Andes, the Australian outback, and Scandinavian tunnels—many of whom have quietly swapped their old bits for these. They mention the same thing: the threads hold, the buttons stay sharp longer, and the total cost per meter drops. It's not a marketing pitch; it's what happens when a factory treats rock drilling tools like precision instruments instead of disposable commodities.
Contact Us
Contact Person: Elma
Email: [email protected]
Tel/WhatsApp: +86 13738628777
Website: https://www.pulankagroup.com/