Pharmaceutical Cleanroom EPC Company Selection Checklist for GMP-Compliant Facilities
2026-11-18
Most GMP cleanroom projects do not fail at the final validation; they inherit problems from the EPC selection stage—inconsistent documentation, overlooked HVAC transitions, or a contractor learning pharmaceutical requirements on your budget. This guide breaks down the selection checklist for pharmaceutical cleanroom EPC partners and shows how a specialist like GENO Pharmatech can change that risk profile before construction starts.
Past Cleanroom Projects Under the GMP Microscope
Looking back at earlier cleanroom builds, the gaps rarely appeared in the final certification reports. They hid in the daily logs, change control records, and the occasional deviation that someone marked “resolved” without describing how. A filling line project from a few years ago stands out: the HVAC design met every static requirement, yet during a routine media fill the operators discovered that opening a pass-through for less than ten seconds was enough to disrupt the pressure cascade.
That single observation triggered a much deeper review. We pulled particle counts at shift changes, compared gowning room traffic against sampling locations, and mapped material flow against air returns. It turned out the real issue was not the air handling system itself, but the way production scheduling overlapped with cleaning windows. The fix was unglamorous—staggered entry times, a revised disinfection rotation, and moving one mobile trolley out of a return air path.
The lesson from those projects is that GMP compliance does not live in a single audit snapshot. It accumulates in how well a cleanroom is operated when nobody is watching. Past projects, once put under the microscope, usually reveal that the most expensive equipment mattered less than the discipline around doors, gowning, and material transfer.
Design-Build Ownership Without Subcontractor Finger-Pointing
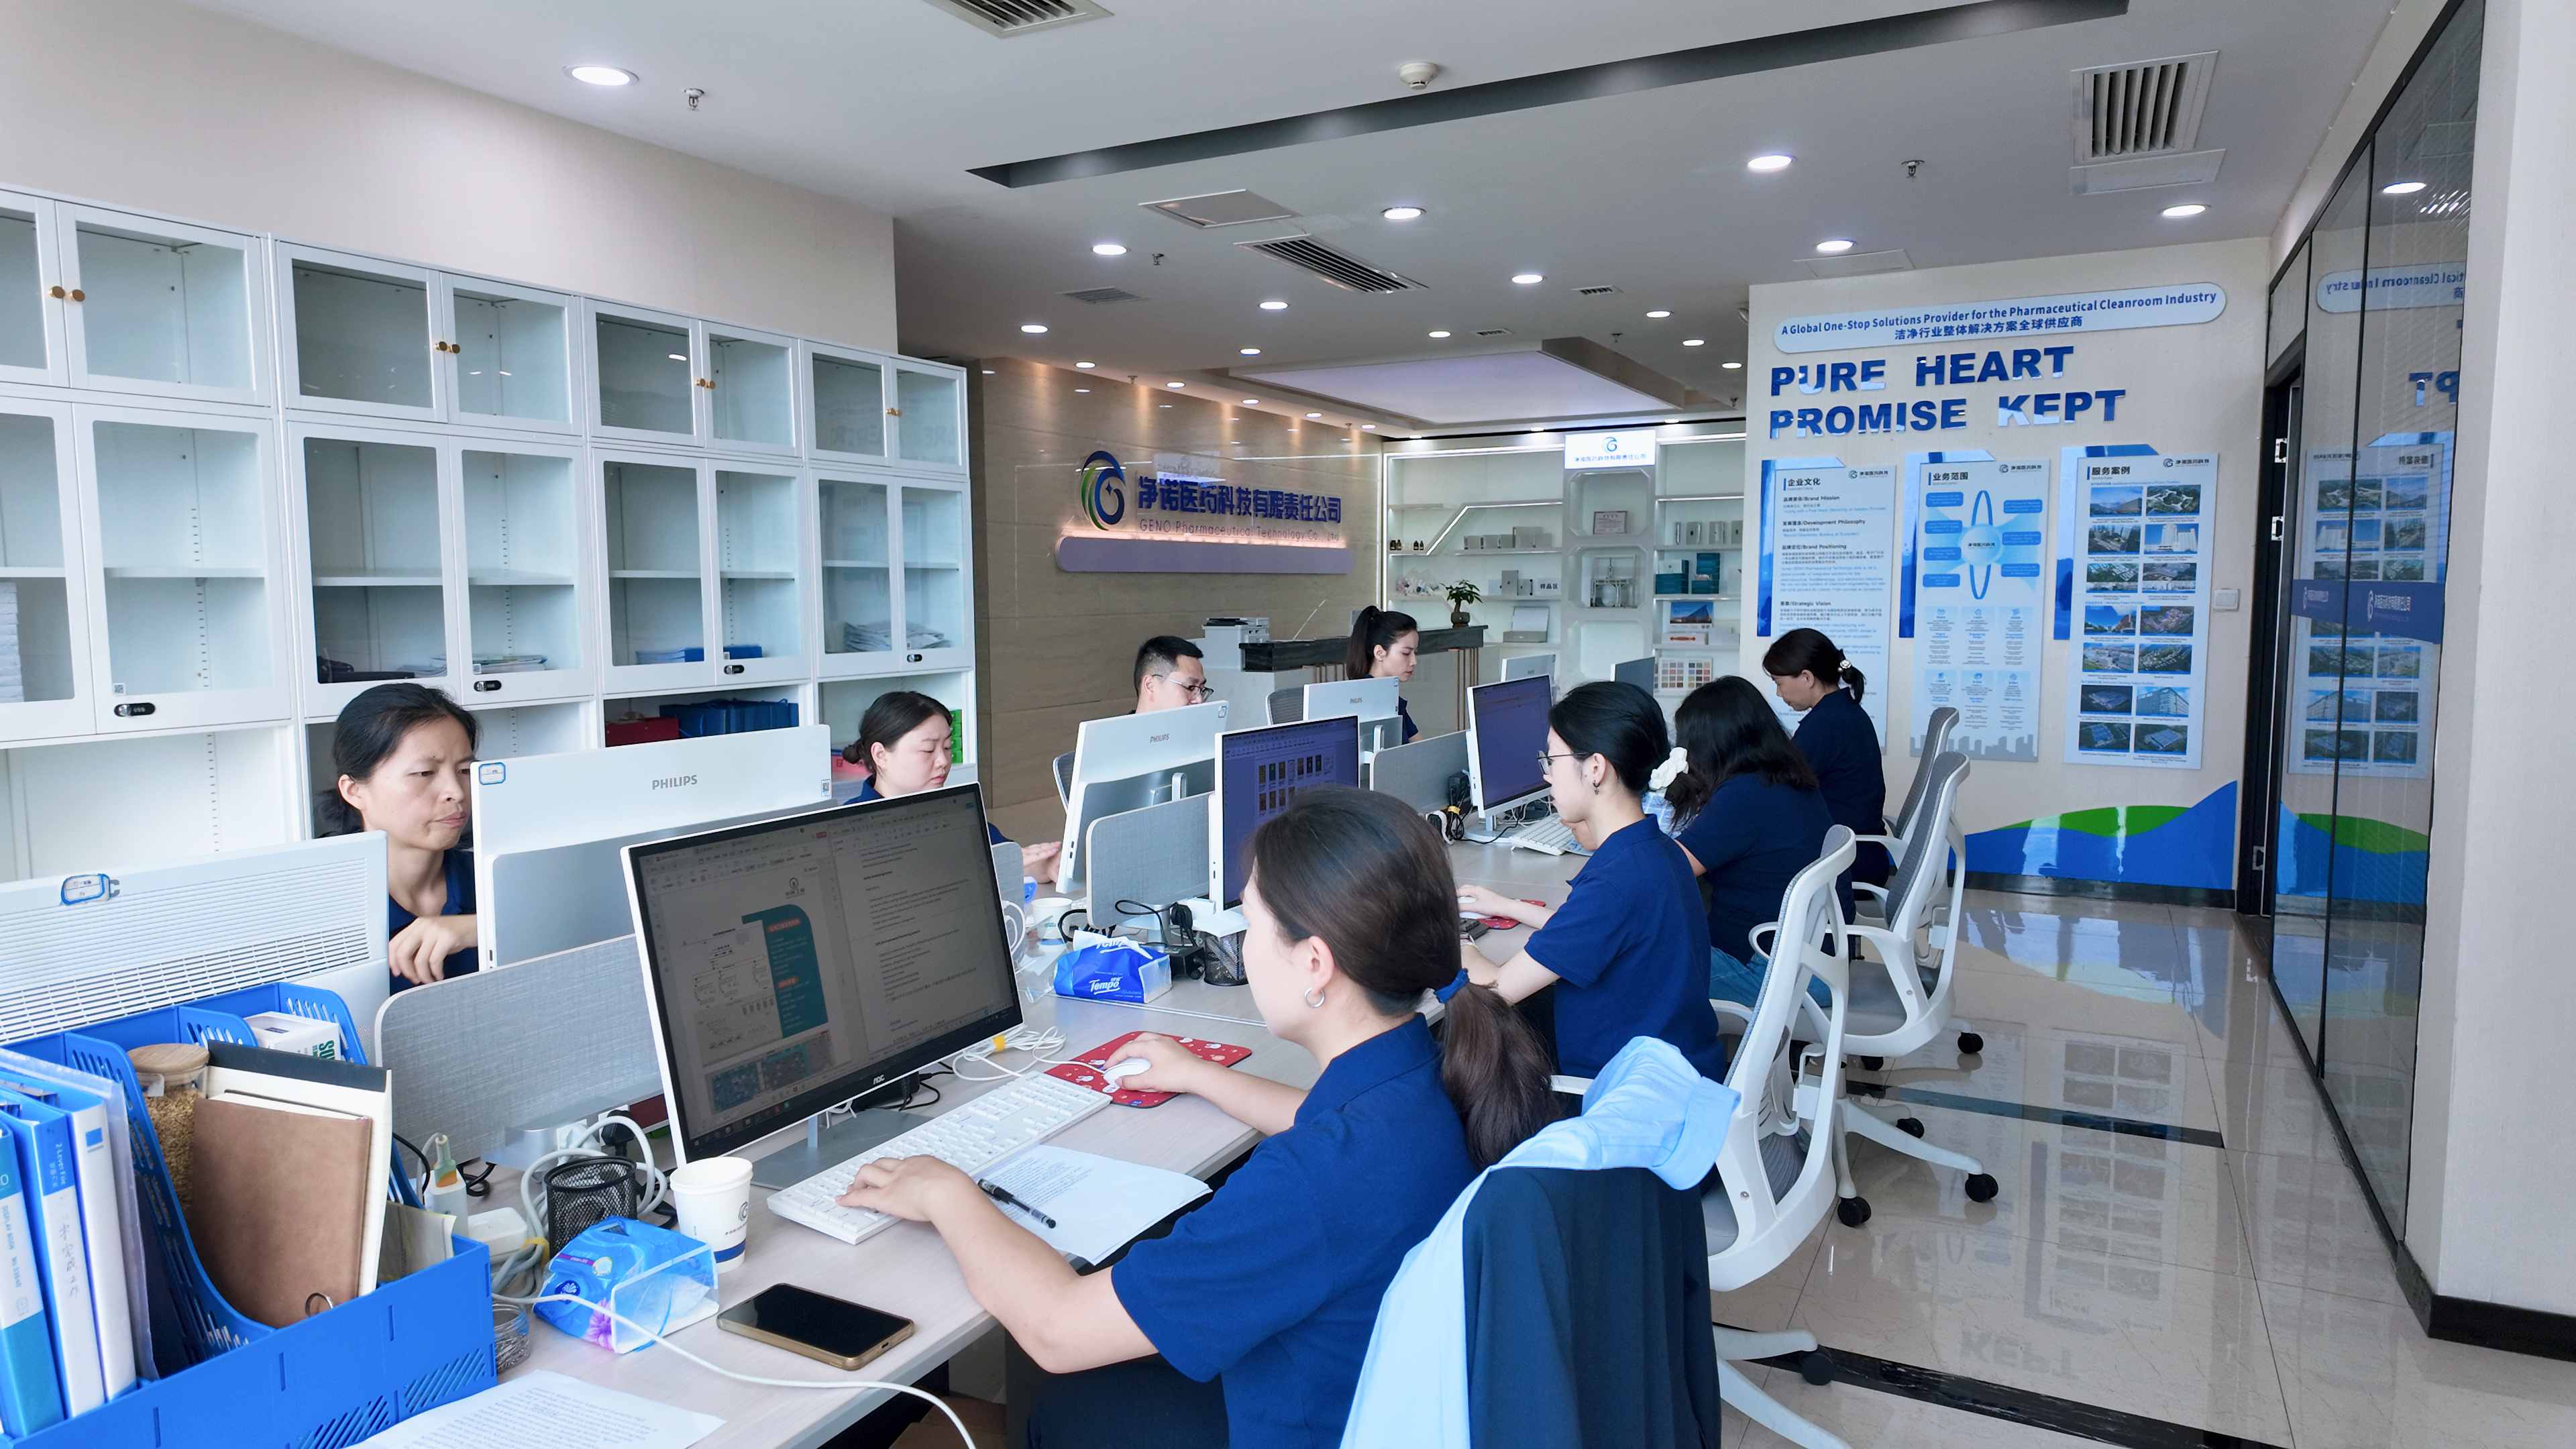
When one team handles both design and construction, the old habit of blaming the subcontractor for every misaligned beam or late material delivery starts to fade. There is no gap between the drawing table and the field trailer, so the people making decisions are also accountable for how those decisions play out on site. That direct line changes the tone of every meeting.
Instead of sorting through a chain of emails to figure out who missed a dimension, you get a single point of responsibility. The team that drew the detail is the same team that pours the concrete or frames the wall. If something does not fit, the fix happens without a formal claim, because finger-pointing now means pointing at yourself.
This approach rewards builders who think like designers and designers who respect buildability. Problems get solved in the trailer at 6 a.m., not in a courtroom six months later. Ownership stops being a legal term and becomes a working habit.
Material Traceability From Wall Panel to Final Wipe
Traceability here starts well before a wipe is cut, sealed, or bagged. Each wall panel entering production carries a lot-level identifier tied to the resin blend, the casting date, and the incoming inspection results for that specific run. That identifier stays attached to the master roll, so any decision made later can still be linked back to the physical panel that started the chain.
When panels move into slitting and converting, the same identifier is recorded at each work order rather than replaced by a generic production date. Operators log which panel sections feed which wipe format, and the resulting sub-lots carry their own trace codes that reference the parent panel. This makes it possible to follow a single finished pack backward through cutting, folding, and wetting without losing the connection to raw material history.
By the time a final wipe reaches its sealed pouch, the lot code on the label acts as a pointer to the full record, not just a batch number. It links back through converting and panel inventory to the original material certification and process data. When a nonconformance appears, the affected range can be narrowed to the exact panel segments and finished lots involved, avoiding broad holds and protecting downstream users.
Commissioning Proof That Goes Beyond Paperwork
A signed checklist rarely tells you how a system actually behaves under load, at partial capacity, or during the handoff from one sequence to the next. Real commissioning proof is built around observed behavior: field measurements, trend logs, damper stroke counts, and sensor readings that line up with the design intent. It replaces the illusion of completion with evidence you can review, question, and trust.
That evidence stays tied to the equipment, not buried in a folder. Time-stamped photos, short clips of valves cycling, before-and-after setpoint trends, and recorded pump curves give each test point a traceable story. If something was exercised, you can see it move. If a reading was taken, you can see the conditions at that moment.
The point is not to produce a thicker handover package. It is to make the system legible to the people who will run it. When the paperwork says one thing and the trend data says another, the data should win. Commissioning proof that goes beyond paperwork gives facility teams something more useful than a signature: a clear, verifiable record of how the building was left performing.
How the Firm Handles Deviation and Rework
When a deviation shows up, the firm treats it as a sorting problem rather than a blame problem. Project leads pull the relevant drawings, specs, and shop notes before deciding whether the affected item can be used as-is, needs rework, or has to be scrapped. That first pass keeps small mismatches from turning into long schedule delays.
Rework is handled through a written sequence, not an ad-hoc fix. The assigned machinist or fabricator gets a marked-up drawing and a clear hold point for inspection. If the same type of deviation appears twice, the quality team digs into the setup, tooling, or material lot to find the source, then updates the checklist so that failure mode is caught earlier the next time.
Anything that affects fit, finish, or structural integrity requires a second sign-off before the reworked item leaves the bench. That second pair of eyes is usually a senior hand who was not involved in the original work. It adds a small delay, but it prevents the much larger delay of a rejected delivery or a return from the field.
Knowledge Transfer That Keeps Your Facility Inspection-Ready
Most facilities don’t fail inspections because the equipment is wrong. They fail because the person who knew the quirks of the fire panel or the backup pump wasn’t on shift that day. That’s the gap real knowledge transfer closes. Instead of handing over a binder that nobody reads, experienced staff walk newer team members through the exact steps they’d take if an inspector arrived at 6 a.m., from checking valve tags to pulling the last three maintenance logs without hunting through a filing cabinet.
We keep that transfer practical and unglamorous. Short walkthroughs, shadowing during actual rounds, quick voice notes for the next shift, and one-page photo guides that show what ‘ready’ actually looks like in your building. The goal isn’t to turn everyone into a compliance expert overnight. It’s to make sure the knowledge lives in more than one person’s head so an audit, surprise visit, or staffing change doesn’t leave you scrambling.
Over time, this becomes part of the routine rather than a training event. A newer operator can point out a ceiling tile that’s slightly out of place or a gauge that’s drifting low because someone showed them what normal looks like on a Tuesday, not just in a seminar. That quiet confidence is what keeps the facility inspection-ready without last-minute panic or a frantic cleanup the night before.
FAQ
They should open with a structured gap assessment against the intended GMP grade, reviewing your process flow, personnel and material flows, HVAC zoning, and finish requirements before proposing any layout. A generic contractor tends to jump straight to partition and ceiling placement.
Look beyond panel brand. Ask for detail drawings showing flush or sealed joints, coved flooring transitions, cleanable surfaces, pressure cascade details, and penetration sealing. Confirm they specify materials with documented chemical resistance to your cleaning and disinfection agents.
Review their air change rate calculations, filter coverage and terminal HEPA placement, temperature and humidity control strategy, pressure differentials across adjacent rooms, and recovery rates after door openings. They should also address low-return locations and as-built duct leakage testing.
Request sample turnover packages from previous projects, not just a qualification protocol template. Ask how they handle change control during construction, weld and inspection logs, pressure test certificates, material traceability, and final as-built drawings tied to room data sheets.
Ask for a detailed containment and phased handover plan. Verify their experience with negative air enclosures, tool cleanliness, sticky mats, boot washes, and scheduled shutdowns. They must define how they protect adjacent GMP areas from dust, vibration, and cross-contamination.
A firm that stops at construction leaves risk in your hands. The right EPC should coordinate cleanroom testing, airflow visualization, filter integrity, room pressure, temperature mapping, and support IQ and OQ activities. Their team should understand regulatory expectations for aseptic or solid dosage environments.
Examine whether they provide a realistic schedule tied to procurement lead times, not an optimistic date. Check their subcontractor management approach, progress reporting cadence, safety record, and how they handle variations when site conditions differ from drawings.
Conclusion
Qualifying an EPC contractor for a pharmaceutical cleanroom starts with pulling apart their claimed project list. Ask for actual GMP case histories that include air pressure cascade failures, recovery times after door openings, and surface particle counts—not just finished-room photos. The most useful references often come from the quality unit rather than the project manager, because they reveal how the cleanroom behaved after handover. A firm that owns design and build under one roof reduces the familiar blame loop between architect, mechanical subcontractor, and commissioning agent. Insist on a single point of accountability when deviations are found, not a chain of emails that ends with the owner managing someone else's scope. Material traceability should run from the wall panel resin and gasket chemistry to the cleanroom wipes used in final cleaning; if a supplier cannot show that chain, it can become an audit finding later.
Commissioning evidence needs to go past static documentation. Walk the installed system with the contractor and have them demonstrate worst-case scenarios: power loss, filter bypass, or a pressure cascade shift. Watch how the firm logs and closes deviations. A healthy EPC partner treats rework as a controlled change, not a hidden patch. The last piece is knowledge transfer that leaves your own team able to explain the HVAC, monitoring, and material flows to an inspector without reaching for the contractor's phone number. That handover should include not only SOPs and drawings but also the reasons behind critical setpoints and alarm limits, so the facility stays inspection-ready long after the project team has left.
Contact Us
Contact Person: Amy Yang
Email: [email protected]
Tel/WhatsApp: 008619330882686
Website: https://www.genopharmatech.com/