Polyurethane Production Line Exporter Guide to Selecting a Trusted Partner
2026-10-25
Choosing a polyurethane production line exporter is rarely just about the equipment. It’s about the partner behind the machinery—their engineering depth, response time, and willingness to stand behind every component. This guide cuts through the sales talk and shows you how to evaluate exporters on the metrics that actually matter, with YI ZHOU TECHNOLOGY serving as a reference point for dependable partnerships.
What a Factory Walkthrough Reveals That Brochures Never Show
Brochures flatten a factory into clean arrows and smiling operators. Walking the floor, you notice the first thing they leave out: the physical rhythm of the place. Conveyors don't hum at one steady pitch; they surge when a batch clears inspection and nearly stall when a labeler jams. The real layout isn't the tidy linear flow on the wall map but a set of workarounds, a pallet staged here because it blocks nothing, a roll of film kept within arm's reach of one particular machine because the auto-feed has been unreliable for years.
The second reveal is how much tacit knowledge lives outside the standard operating procedures. A line leader adjusts the heat-seal temperature by sound, not by the digital readout. An operator nudges a guide rail with a folded piece of cardboard to stop a recurring skew. None of that appears in the official training deck, and each shift guards its fixes. Brochures show the automation, but the walkthrough shows the quiet human calibrations that keep the automation from drifting out of tolerance.
You also see the material truth behind the output numbers: the pile of rejected lids that will be reground, the corner where a leaking drum was caught before it reached the drainage grate, the board with handwritten torque checks that hasn't been updated since Tuesday. These are not failures in the brochure sense; they are the factory's immune system. A glossy page can list zero-defect goals. The floor shows you how much vigilance and informal repair it actually takes to get close.
Questions to Ask About Mixing Head Calibration and Maintenance
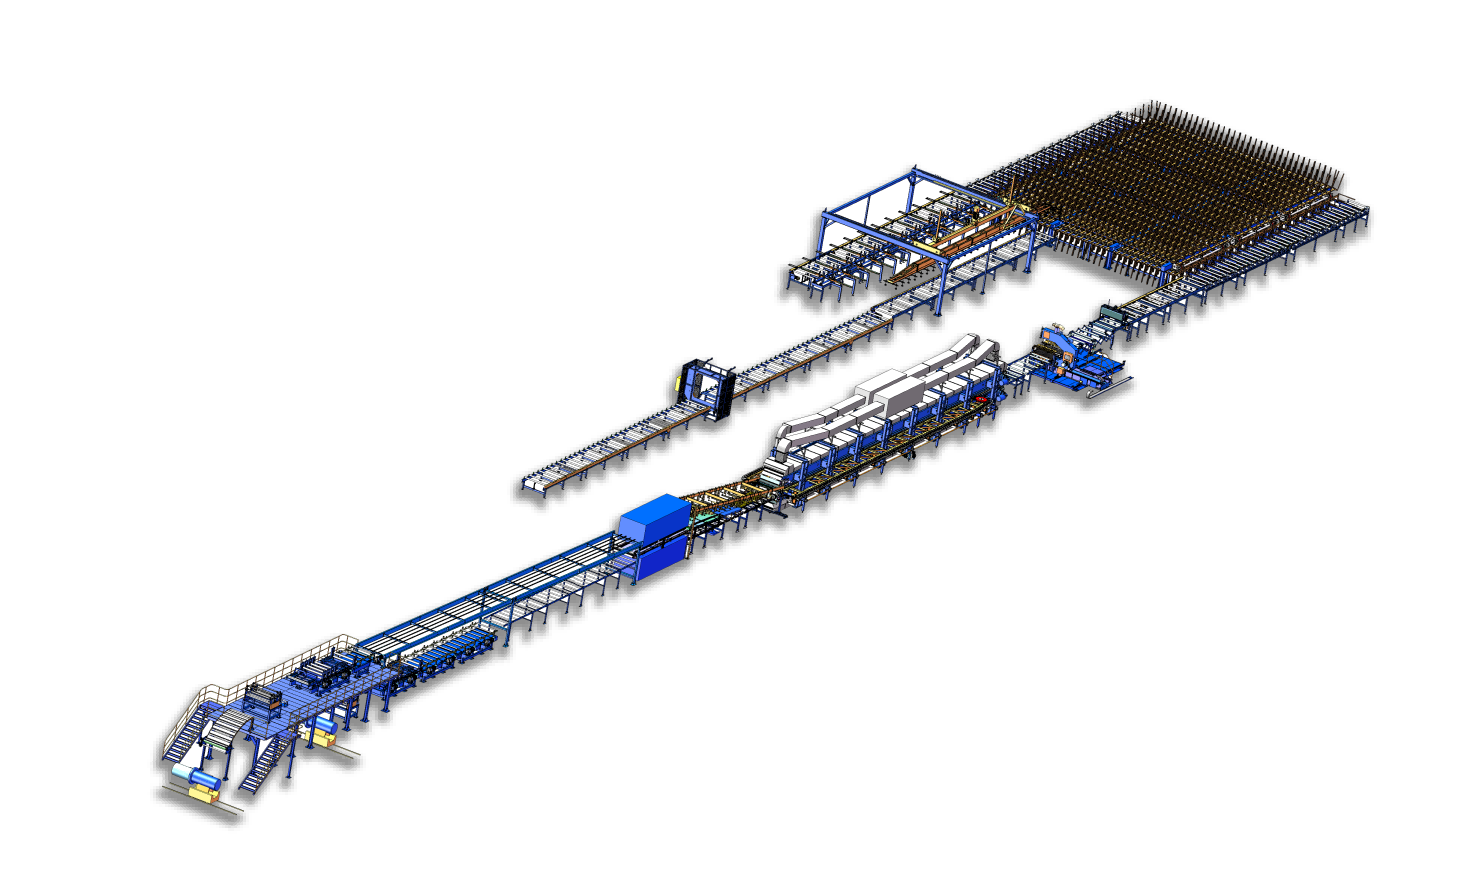
When the mixing head starts showing inconsistent shot weights or off-ratio resin, the first thing to pin down is whether you’re chasing a calibration drift or a mechanical wear issue. Ask your maintenance lead what the last recorded baseline was for stroke position, counter-pressure, and temperature at the nozzle. Without those numbers, any quick adjustment tends to hide the real problem for another week.
Another question that rarely gets asked early enough: which internal seals and needle tips have actually been replaced in the last six months, and does the service log separate cleaning from true recalibration? A worn mix chamber liner can mimic a calibration fault, so confirming whether the head was rebuilt or just flushed changes the whole troubleshooting path.
Finally, ask how adjustments are logged and verified between shifts. If the night crew tweaks the zero point without noting the ambient temperature or material lot, you’ll end up re-solving the same issue every Monday. A practical question is whether the team can pull up a before/after snapshot of the head’s response curve, not just a checkbox saying ‘calibrated’.
The Hidden Cost of Ignoring Your Raw Material Viscosity Range
Viscosity slips under the radar because it rarely trips an alarm on day one. A batch that's slightly thicker than spec still pumps, still mixes, still gets packed—but it leaves a quiet trail of extra energy draw, longer cycle times, and strain on pumps and seals that maintenance teams write off as normal wear. Over a quarter, those “minor” deviations turn into a measurable jump in unplanned downtime and replacement parts that never gets traced back to the source.
Then there's the quality drift that happens when operators compensate on the fly. They might thin a coating with solvent, adjust a fill temperature, or slow a line to keep rejects down. Each workaround masks the true problem and creates a new one: scrap rates creep up, rework becomes routine, and two batches of the same product no longer behave the same for the end user. The cost isn't a single line item—it's scattered across returns, customer complaints, and lost repeat orders.
The most expensive version of this problem shows up in audits or when a new supplier changes the viscosity profile without anyone noticing. Suddenly a process that ran fine for years starts producing off-spec output, and troubleshooting eats weeks because nobody thinks to check the raw material first. That delay, plus the overtime and expedited shipments needed to recover, often outweighs the savings from accepting a wider viscosity range in the first place.
How to Test an Exporter's Problem-Solving Instincts Before You Pay
A supplier who only shines when everything goes smoothly tells you nothing about their real character. Before you wire a deposit, introduce a small, controlled complication: ask them to verify a non-standard tolerance, clarify how they would handle a delayed raw material batch, or suggest a better packing method for your specific port conditions. Watch whether they ask clarifying questions, push back with evidence, or simply say "no problem" and move on. The last response is the riskiest; it often means they haven't thought through the actual constraints and will figure it out only after your money is gone.
You can also run a live problem-solving exercise during the negotiation itself. For instance, send a short message on a Friday evening their time and ask for a revised quote with a slightly different product spec by Monday morning. Don't demand speed for its own sake; instead, look at how they structure the answer. Do they flag the one cost driver you hadn't mentioned? Do they offer two viable options instead of one? Do they ask about your end-use environment rather than just confirming the change? If the reply is a single word or a generic reassurance, treat that as a data point about how they'll behave when something actually breaks.
Finally, always pair these tests with a check on how they treat mistakes. Give them an opening to correct a small error you deliberately plant in the order details, like a mismatched HS code or an outdated drawing revision. A strong exporter will catch it before you do, explain the potential customs delay, and propose a fix without turning it into a drama. A weak one will either ignore it, agree with it to please you, or blame an invisible team member. The goal isn't to trap them; it's to see if their default response under pressure is to solve the problem or to protect their own position. That instinct is what you're actually paying for.
Why Their Spare Parts Warehouse Tells You More Than Their Catalog
A catalog is a carefully staged performance. Every page is polished, every part number sits in neat rows, and every specification reads like a promise. But walk into the spare parts warehouse and you step behind the curtain. The shelves tell a different story: which components are actually pulled off them day after day, which ones have gathered a thin film of dust, and which bins have been hastily relabeled more times than anyone cares to admit. The warehouse doesn't sell you an image—it reveals the machine's true appetite.
Look at how the space is organized. Are critical parts kept within arm's reach of the dispatch area, or buried in a far corner behind obsolete inventory? Does the labeling system speak of a single clear logic, or has it grown like patchwork over years of emergency fixes? A company that maintains a coherent, navigable warehouse is usually one that understands its equipment's failure patterns. A chaotic one, no matter how glossy the catalog, is likely spending too much time searching for parts and too little time preventing the next breakdown.
Most telling of all is the inventory itself. A healthy spare parts stock balances redundancy against obsolescence. Too many of the same critical component might hint at repeated, unresolved failures. Too few, and you're looking at a company that gambles on uptime. The warehouse is a physical ledger of real-world usage, unfiltered by marketing language. You can learn more from a ten-minute walk down its aisles than from a hundred pages of product descriptions.
The Difference Between a One-Time Installer and a Process Partner
A one-time installer shows up, completes the agreed scope, and then moves on to the next job. The work might be technically sound, but once the invoice clears, you are on your own. This arrangement works when the task is isolated and the requirements are unlikely to shift.
A process partner, by contrast, treats the initial setup as the starting line rather than the finish. They stay involved through the messy middle: tracking how the solution behaves under real conditions, catching small issues before they become expensive ones, and adjusting the approach as your operations change. Their value is not in a single handoff but in the accumulated fixes, refinements, and conversations that happen afterward.
The practical difference shows up in accountability. The installer owns the installation. The partner owns the outcome over time. One is measured by completion; the other by whether the result still works months down the road.
FAQ
Start by looking at their track record with projects similar to yours, not just the number of years they have been around. Request case studies or references from actual clients and ask about specific challenges they solved. A trustworthy exporter will be transparent about past installations, including performance data and any delays encountered, rather than only sharing glowing testimonials.
Ask for detailed engineering drawings, component specifications, and a bill of materials with brand names of critical parts like pumps, mixers, and control systems. Then cross-check those parts with independent suppliers or online industrial forums. A partner who hesitates to name third-party component brands or provides vague data sheets may be hiding low-grade substitutions.
Polyurethane lines are complex and downtime is expensive, so the real test comes after installation. Inquire about their typical response time for remote diagnostics, whether they have local service engineers or partners in your region, and how they handle warranty claims. Strong exporters often offer training for your operators and a structured maintenance schedule instead of leaving you to figure out faults yourself.
Avoid companies that push a standard line without asking about your raw material types, desired output rate, foam density range, or factory layout constraints. A dependable partner will ask many questions first, then propose modifications to mixing head design, conveyor length, or temperature control. Request a detailed technical proposal that references your actual production goals rather than a generic brochure.
Look for CE marking if you import into Europe, ISO 9001 for quality management, and relevant electrical or safety certifications like IEC standards for control panels. Beyond certificates, ask how they ensure machines meet local voltage, emission, and workplace safety rules. A partner who understands your country's import regulations and can provide pre-shipment inspection reports demonstrates serious professionalism.
Be cautious if they avoid sharing client contacts, refuse a factory audit or video tour, demand full payment before production starts without a milestone plan, or quote significantly lower than market average without explanation. Also watch for inconsistent answers about delivery lead times or component origins. Reliable suppliers welcome scrutiny and provide clear contracts with penalty clauses for delays.
Polyurethane machinery uses wear parts like mixing chamber seals, filters, and metering pumps that need regular replacement. If the exporter cannot guarantee a stock of critical spares or has no system for fast international shipping, your line could be idle for weeks. Ask for a recommended spare parts list with prices and lead times upfront, and confirm they still support equipment produced years ago.
Engage their engineers in a technical discussion about your specific formulation, such as how they would handle high-viscosity polyol or abrasive fillers. A knowledgeable partner will discuss pump sizing, temperature conditioning, and mixing pressure in detail. If their sales team only repeats marketing phrases or cannot explain the difference between low-pressure and high-pressure dispensing, that's a clear signal to look elsewhere.
Conclusion
A factory walkthrough reveals what brochures never show: real calibration records, mixing head cleanliness, and whether maintenance is scheduled or only reactive. Ask pointed questions about how often they calibrate the mixing head and what happens when raw material viscosity drifts outside the specified range. Ignoring that viscosity range quietly ruins foam quality, wastes chemicals, and shortens pump life, so a competent exporter should discuss it without being prompted. Their spare parts warehouse is another place where talk falls apart; a deep, organized stock of seals, filters, and sensor components tells you they expect to support you for years, while a thin shelf of miscellaneous boxes says they sell and run.
Before you pay, create a low-stakes problem—like a sudden viscosity change or a clogged mixhead—and see how the exporter responds. Do they ask about your line speed, temperatures, and raw material batch, or do they just offer a new part? That instinct separates a one-time installer from a process partner. The installer finishes the job and leaves; the partner stays engaged with training, remote diagnostics, and regular check-ins. Choose the exporter whose warehouse, walkthrough, and reaction to pressure show an engineer's mindset rather than a sales script, because that is the partner who will keep your polyurethane line running when conditions are no longer perfect.
Contact Us
Contact Person: Sophia Jiang
Email: [email protected]
Tel/WhatsApp: +86 17367381818
Website: https://yzwelding.com/