Sintered Silicon Carbide Supplier Guide: Key Qualities to Evaluate Before Partnering
2026-09-27
Sintered silicon carbide shows up in critical components—pump seals, semiconductor chucks, armor tiles—but not every supplier delivers the same reliability. One overlooked impurity or an inconsistent sintering run can turn a promising design into a field failure. So how do you evaluate a partner before you’re locked into a contract? This guide walks through the qualities that actually matter: raw material purity, density control, dimensional tolerance, and post-sintering support. And if you want a concrete benchmark for comparison, HUAYI TECH has built its reputation on precisely these metrics—worth a close look before you finalize your shortlist.
The purity data that actually predicts wear life in silicon carbide
Most datasheets list total purity as a single number, but that figure alone tells you almost nothing about how long a silicon carbide seal face will survive under abrasive conditions. What really matters is the concentration of free silicon and residual carbon left over from the reaction bonding process. Free silicon is soft and wears away quickly, creating micro-pits that accelerate erosion of the surrounding hard grains. Residual carbon, if clustered rather than uniformly dispersed, acts as a crack initiation site under cyclic loading. A difference of just 0.5 percent in free silicon content can cut wear life by a factor of two in high-velocity slurry service.
The predictive power lies in quantifying the ratio of alpha-phase to beta-phase silicon carbide combined with impurity mapping across the cross-section. Bulk chemical analysis averages out local inhomogeneities, but wear initiates at weak spots. Microprobe scans that reveal silicon-rich pockets or carbon agglomerates near the wear surface give a far better indication of long-term performance than a certificate stating 99.5 percent pure. We have tracked dozens of field failures where the material met the nominal purity spec yet showed premature grooving because the impurities were concentrated in bands parallel to the sealing face.
A more useful dataset includes not just total impurity concentration but also the grain boundary chemistry. Trace amounts of iron, aluminum, and calcium from sintering aids can form glassy phases at grain boundaries. These phases soften under frictional heating, allowing grains to pull out rather than wear gradually. When you plot grain boundary glass phase volume fraction against measured wear rate in a standardized slurry test, the correlation is strong and reproducible. That is the purity data worth requesting from suppliers — not the headline number, but the spatial distribution and chemical speciation of what should not be there.
Sintering curves reveal batch consistency better than any density number
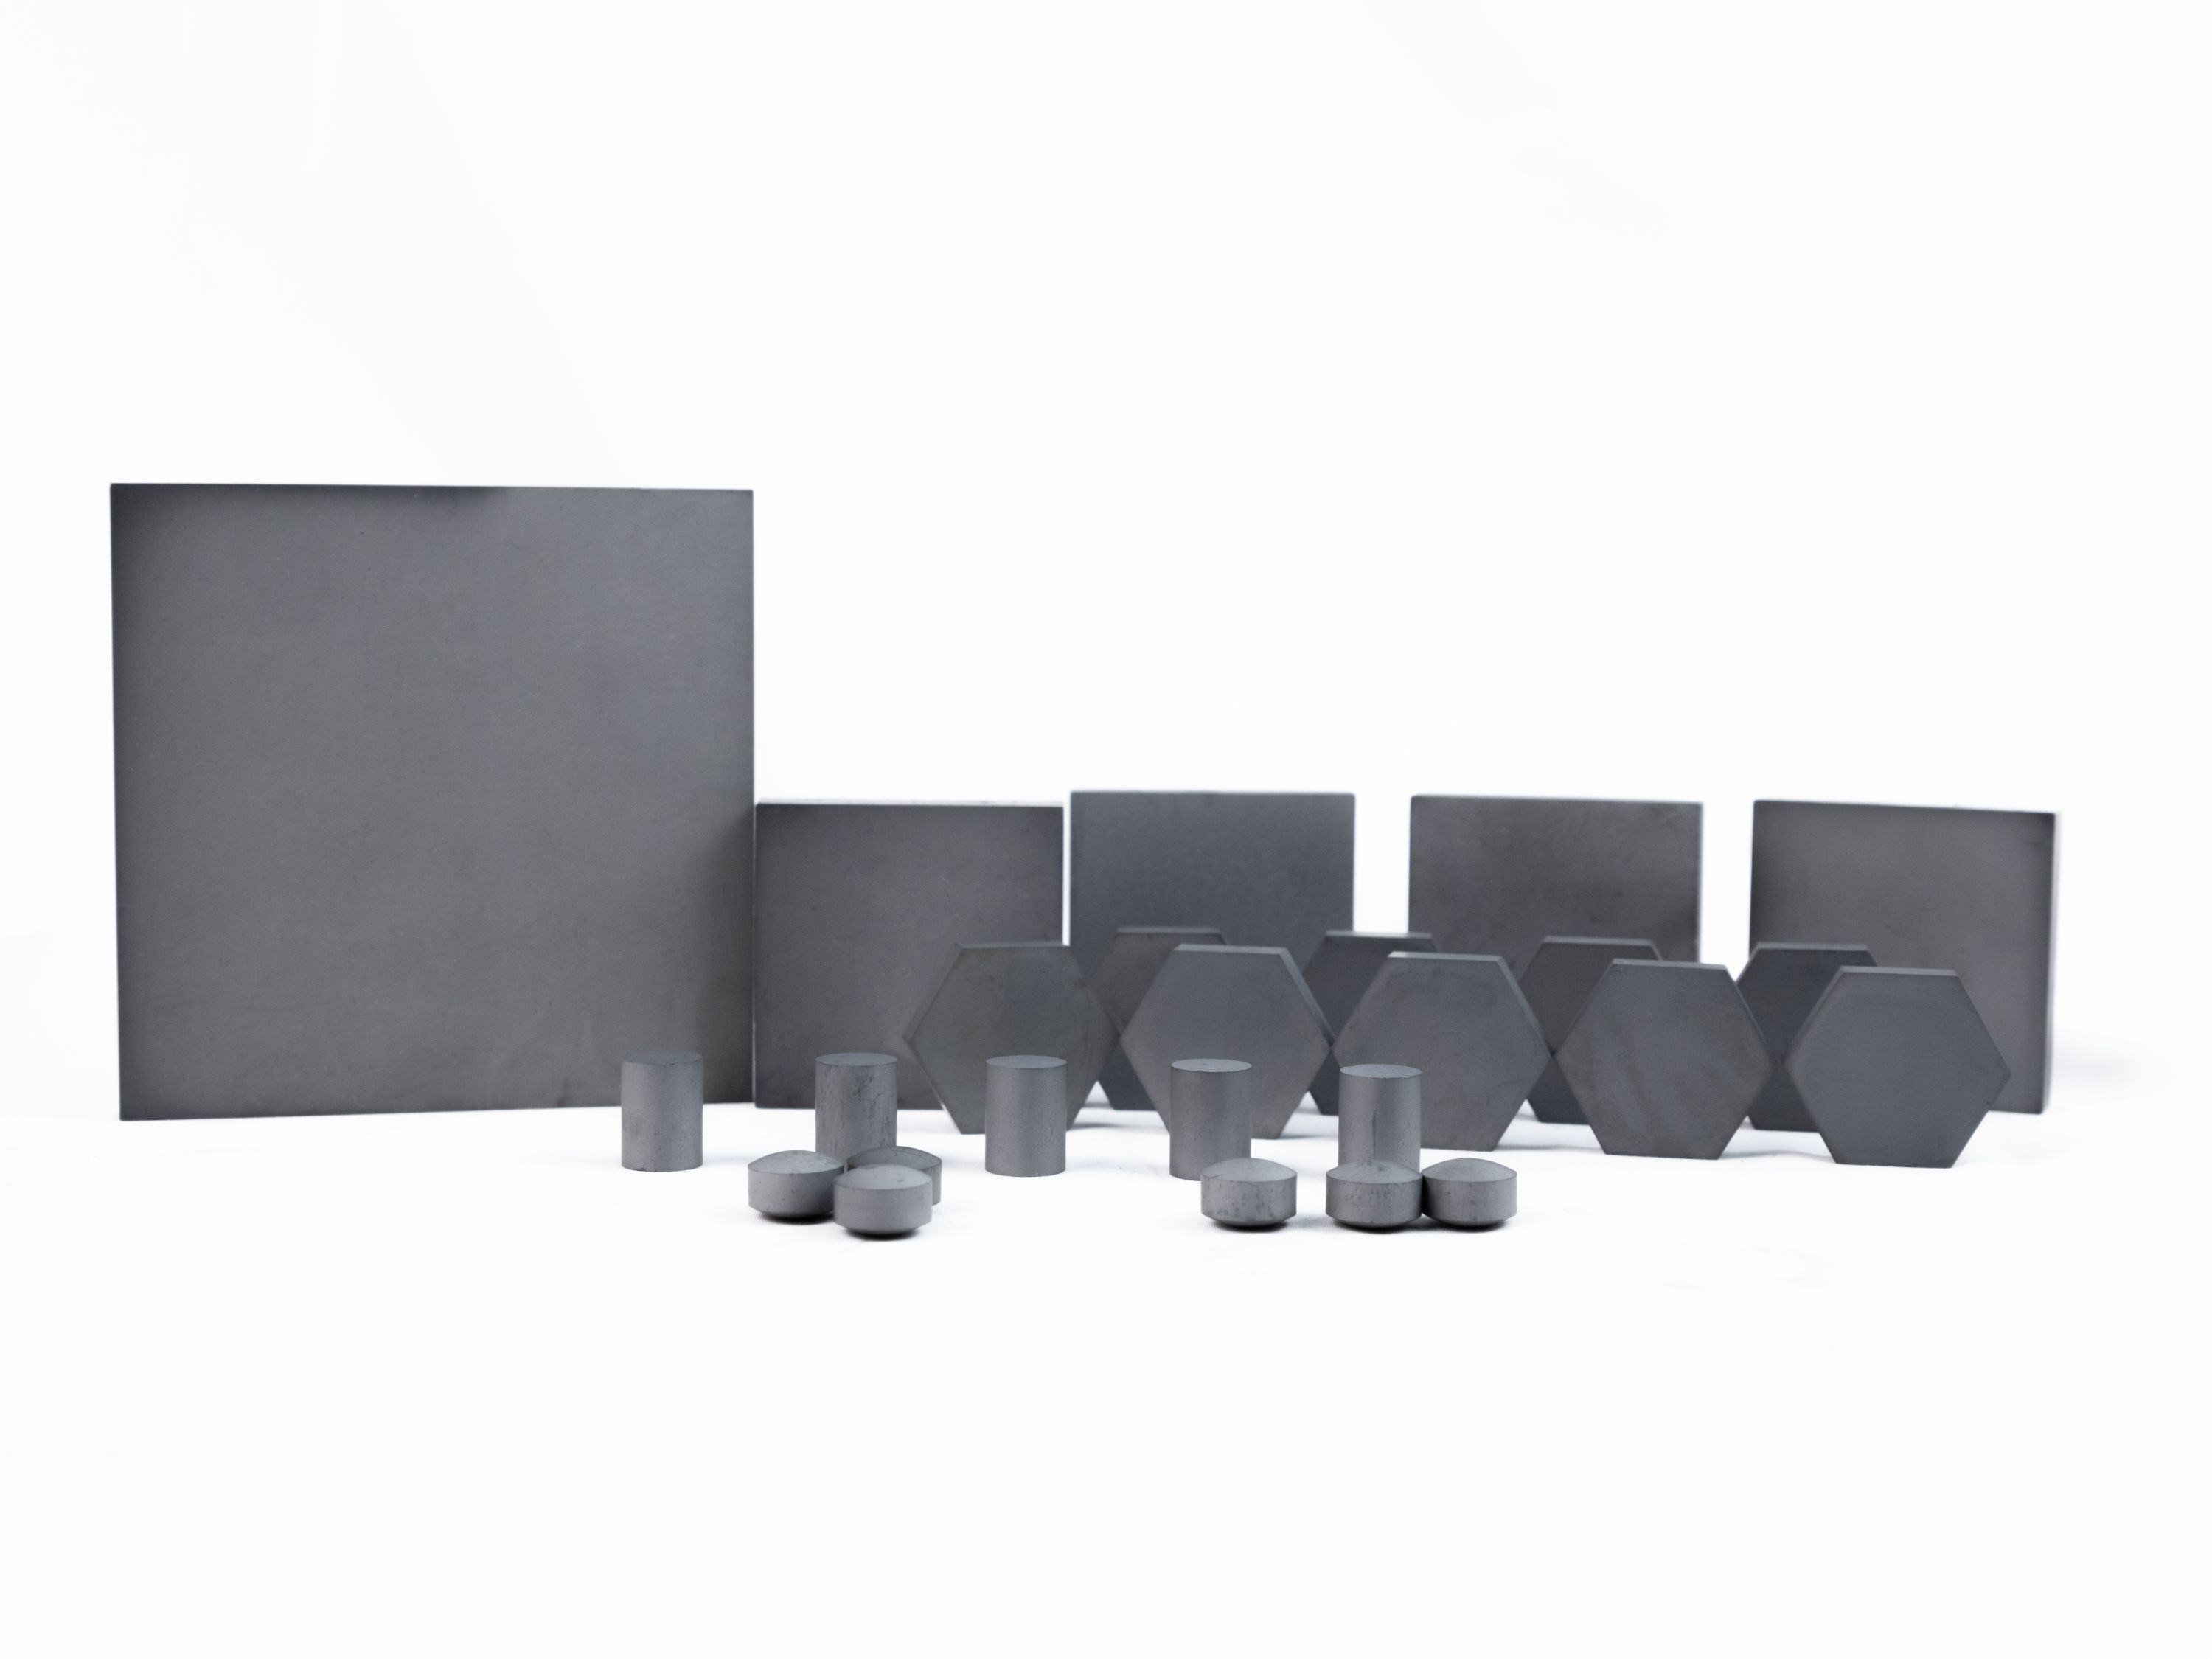
A single density value—say 7.85 g/cm³—tells you almost nothing about how a powder compact actually behaved in the furnace. Two batches can hit that exact number and still differ wildly in the path they took to get there. One might densify early, hold a stable plateau, and then shrink another half percent during cooling; the other might lag until the last hundred degrees, then rush through final-stage sintering with uncontrolled grain growth. Only the full sintering curve, tracking shrinkage, shrinkage rate, and temperature in real time, exposes those differences.
When you overlay curves from several production lots, batch consistency becomes visible at a glance. The shape of the curve—where the inflection points sit, how steep the main shrinkage event is, whether there's a secondary bump—acts like a fingerprint for the raw powder and the pressing conditions. A density number can't show that one batch entered the sintering window 20°C later than the others, or that another had a broader, more sluggish densification profile. If the curves sit tightly together, you have a stable process; if they fan out, you have a problem that no final density check will catch.
Mechanical strength claims should match your real component stress state
Designers often rely on generic material datasheet values when claiming mechanical strength, but those numbers rarely reflect the complex stress state a real component experiences under load. A simple tensile test specimen, for instance, sees uniaxial stress, while your bracket may undergo combined bending, torsion, and contact pressure. Ignoring this mismatch leads to overly optimistic strength claims that can fail in the field.
To align your strength claim with reality, start by mapping the actual stress distribution in the component using finite element analysis or strain gauge measurements. Then compare the maximum equivalent stress—such as von Mises for ductile materials—against the material's true strength under similar loading conditions. This approach ensures the stated mechanical strength corresponds to the part's genuine load-bearing capacity rather than an idealized coupon test.
Finally, consider environmental and manufacturing factors that alter stress state, such as residual stresses from welding or machining, or stress concentrations at fillets and holes. Validating your claim with prototype testing under representative loading conditions closes the gap between datasheet strength and component performance, giving you a defensible mechanical strength specification.
Final tolerances are decided at the green machining stage, not just grinding
In ceramic and powder metallurgy manufacturing, there's a persistent assumption that grinding is where final tolerances are locked in. But that overlooks how much dimensional control is already set during green machining. The unsintered compact is soft enough to cut with standard tooling, yet any variation in green dimensions gets amplified by sintering shrinkage. If the green part is off by a few microns, the sintered part can be off by considerably more once the shrinkage factor is applied.
That's why modern process engineers treat green machining not as a roughing step but as the primary stage for establishing near-net shape. Shrinkage rates are predictable, but only if the green stock is uniform and the machining parameters stay consistent. A tolerance of ±0.5% on a green dimension might translate to a much tighter band on the fired part—provided the green machining itself doesn't wander. Waiting until grinding to correct these errors often means removing too much material or risking microcracks in the sintered layer.
The result is a shift in where responsibility sits. Grinding remains essential for surface finish and final micro-adjustments, but it's no longer the sole arbiter of tolerance. By the time a part reaches the grinding wheel, its dimensional fate has largely been decided. Getting the green stage right reduces grind stock, shortens cycle time, and avoids the costly surprises that come from trying to fix sintering distortion after the fact.
A supplier's corrective action speed shows more than any quality certificate
When a batch arrives with defects, the clock starts. A supplier that can trace the root cause, quarantine affected stock, and ship replacements within days tells you more about their operational health than any wall of framed certificates. Paper audits capture a moment; corrective action reveals whether the system actually breathes.
Speed here isn't about rushing a band-aid. It's about having clear escalation paths, empowered quality engineers, and honest data collection already in place. Suppliers who drag their feet often lack these fundamentals—they hide behind emails, request more samples, or argue about tolerance instead of fixing the line. That delay costs you production hours and customer trust.
Next time you evaluate a vendor, skip the glossy compliance folder for a minute. Ask for their last three non-conformance reports and the time from detection to verified closure. The answer will forecast your future headaches better than any ISO stamp.
Delivery reliability needs buffer stock behind the promised lead time
When you promise a customer an exact delivery date, you're essentially making a bet on every step of your supply chain running flawlessly. The problem is that real operations rarely work that way. A supplier misses a shipment by a day, a machine breaks down during peak production, or a freight carrier gets rerouted due to weather. Without buffer stock sitting behind your promised lead time, any of these small hiccups instantly turns into a missed delivery and an unhappy customer. Buffer stock acts as a shock absorber, giving you the breathing room to absorb variability without breaking your public commitment.
Think of buffer stock not as excess inventory, but as insurance against the unexpected. Most companies plan their lead times based on average conditions, but averages hide the messy reality of delays and demand spikes. If your average production time is five days, you might promise delivery in seven days to appear competitive. But if a key component arrives two days late, that cushion of two days is gone and you're already behind schedule. Placing buffer stock behind the promised lead time means you can still ship on time even when your internal processes fall behind, because the finished goods are already sitting in the warehouse, waiting for the order to come in.
There's also a psychological aspect to consider. When a company consistently delivers on time, customers start to trust that promise and may even reduce their own safety stock, relying on your reliability. But that trust is fragile—one late order can trigger a chain reaction where the customer places orders earlier or switches suppliers. Buffer stock behind the lead time allows you to decouple the customer-facing promise from your internal production reality. You can maintain a fast quoted lead time while internally using a longer planning horizon, effectively using inventory to buy time and protect the relationship. The alternative—promising only what you can guarantee under worst-case conditions—makes you look slow and uncompetitive in the market.
FAQ
Ask for a full density report using Archimedes method, not just a nominal value. Also request flexural strength data from three-point or four-point bending tests at the actual operating temperature, not room temperature alone. If the parts will face acidic or alkaline conditions, ask for corrosion weight loss figures in the specific chemical environment. Many suppliers only share generic datasheets; insist on batch-specific results with traceable lot numbers.
Look at the variation across multiple production lots. Request Cpk or process capability data for density and hardness over at least 12 consecutive batches. A supplier that can show a Cpk above 1.33 for density has a repeatable furnace cycle. Also ask about their sintering atmosphere control, whether they monitor pressure and temperature in real time and adjust for seasonal humidity changes in the powder handling room.
Free silicon and residual carbon are the two big ones. Too much free silicon reduces high-temperature strength and oxidation resistance, while excess carbon can cause porosity and lower hardness. For demanding applications, ask for free silicon below 0.5% and total carbon within 29-30% for reaction-bonded grades. Trace metals like iron and aluminum should stay under 0.05% combined because they form low-melting phases at grain boundaries.
Request a polished cross-section micrograph and measure the average grain size yourself or through a third party. In fine-grained SiC, grain sizes below 5 microns typically give better wear resistance and higher fracture toughness. Beware of bimodal distributions where a few large grains act as crack initiation sites. Also ask whether the supplier uses alpha or beta SiC as the starting powder, since beta converts to alpha during sintering and can create elongated grains that help or hurt depending on the application.
ISO 9001 is a baseline but tells you little about ceramic-specific control. Look for IATF 16949 if the parts go into automotive or heavy-duty diesel applications, it forces much tighter process discipline. For semiconductor or chemical processing components, ask for batch-level chemical purity certificates and particle cleanliness data. Some suppliers also follow ASTM C1421 for fracture toughness testing; if they can provide those numbers voluntarily, it signals they understand failure modes rather than just manufacturing.
Set a material fingerprint at the qualification stage using X-ray diffraction (XRD) and scanning electron microscopy (SEM) with energy-dispersive X-ray spectroscopy (EDS). Then require the same fingerprint report with every shipment. If the alpha-to-beta phase ratio shifts or new trace elements appear, the powder source likely changed. Also include a clause that any process or raw material change requires re-qualification and written approval before shipping. Cheap suppliers often switch to recycled SiC powders that carry unknown contaminants.
The supply chain for high-purity SiC powder is concentrated in a few regions, and some grades require specialized milling equipment that cannot be quickly replicated. Ask whether the supplier has at least two qualified powder sources and how much safety stock they hold for critical raw materials. Also check their furnace capacity, if they rely on one large sintering furnace, a single refractory failure can halt deliveries for months. Finally, ask about their graphite crucible and setter plate sourcing because those wear parts are often overlooked but can cause contamination if switched to a cheaper supplier.
Conclusion
In evaluating a sintered silicon carbide supplier, the usual glossy brochures matter far less than a few overlooked details. The purity data, for example, should be tied directly to expected wear life in your application—impurities like free silicon or trace metals will quietly undermine performance even when the nominal grade sounds right. You also want to see the sintering curve, not just a final density number; the shape of that curve tells you whether the supplier’s batches actually behave consistently from lot to lot. Mechanical strength figures only mean something if they reflect the stress state your component will actually see, so ask for data at the relevant temperature, loading mode, and surface condition rather than a polished flexural number. And final tolerances are mostly set before the part ever reaches the grinding room; look for a supplier that treats green machining as a precision step, not an afterthought.
Beyond the technical specs, the way a supplier responds when something goes wrong is often the clearest signal of their real quality system. A certificate on the wall does not fix a missed shipment, but a fast, honest corrective action process does. Ask for a recent example of a nonconformance and how quickly they contained it, traced the root cause, and verified the fix. On delivery, a quoted lead time means little without buffer stock behind it. The best suppliers keep safety stock on commonly ordered grades and can absorb a sudden demand spike without making your production line wait. Taken together, these points give a far more reliable picture than a spec sheet alone.
Contact Us
Contact Person: Junting Leo
Email: [email protected]
Tel/WhatsApp: +86 18615009766
Website: https://www.huayimaterial-china.com/